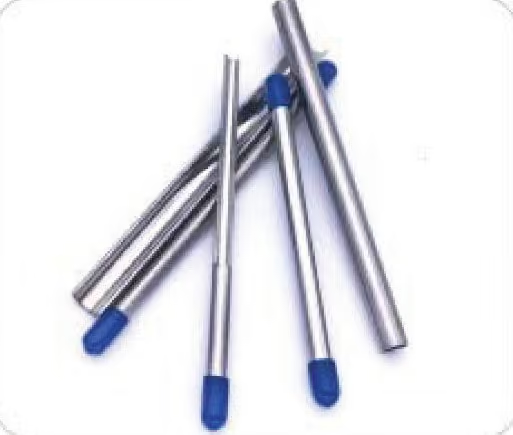
Bright annealed tubing — BA tube — is stainless tubing whose final heat treatment happens in a closed furnace under hydrogen or vacuum, so the metal never oxidizes and exits bright, clean and unpickled.
That single process difference changes the surface chemistry, the cleanliness and the sealing behavior of the tube — which is why instrumentation and high-purity systems specify it almost by default.
It is specified because the surface is what a ferrule bites and what an analyzer line has to live with. BA surface roughness runs Ra 0.04–0.6 µm depending on grade, against ~0.9–1.4 µm for pickled tube.
The catch: ASTM A269 does not fix a Ra value, so the finish belongs on the purchase order, written out.
Key takeaways
- Standard annealing happens in air and leaves oxide scale that must be pickled off; bright annealing happens in a hydrogen or inert atmosphere, so no scale forms, no pickling is needed, and the passive chromium-oxide layer stays intact.
- The payoff is measurable: BA surfaces run roughly Ra 0.04–0.6 µm depending on grade, versus ~0.9–1.4 µm for pickled tube — a smoother, more corrosion-resistant surface that also gives compression ferrules a consistent, clean bite.
- BA tube is normally written to ASTM A269 — but A269 alone does not mandate a Ra value, so the purchase order must state the finish explicitly (for example, ID Ra ≤ 0.4 µm) or two “A269 BA” deliveries can differ wildly.
Which tube does this line need?
Start with what the surface has to do. Where nothing downstream cares about roughness — general hydraulics, plant utilities — standard annealed tube is the correct buy. Where a ferrule bites the OD or an analyzer sees the ID, the finish becomes a specification line.
| Finish | Typical ID Ra | Where it lands | What decides it |
|---|---|---|---|
| Standard annealed, pickled | ~0.9–1.4 µm | General hydraulics, plant utilities | Surface cleanliness is not a requirement and the budget rules |
| BA, standard grade | around Ra ≤ 0.6 µm | General instrumentation | The ferrule bite and a chemically quiet ID |
| BA, precision | ≤ 0.4 µm | Pharmaceutical and food contact | Cleanability is written into the specification |
| BA, ultra-high-purity | ≤ 0.25 µm | Semiconductor and UHP gas service | The process tolerates a narrower roughness band |
The narrowest band, ≤ 0.25 µm, is written for semiconductor and ultra-high-purity gas service.
All four rows are the same argument at different tolerances: how much roughness the service will accept. The line between them is a finish, not an alloy, and it is the one line an A269 certificate does not draw.
What changes in the furnace?
Standard tube is annealed in open or combustion atmospheres. Oxygen attacks the surface, and the tube leaves the furnace carrying oxide scale that has to be removed.
That removal is pickling: an acid bath strips the scale, roughens the surface and damages the corrosion-protective oxide layer, which must then be passivated back. The surface that returns is clean, but it is no longer the surface the furnace made.
Bright annealing replaces the air with a controlled atmosphere of hydrogen or inert gas in a closed furnace. The tube heats, recrystallizes and cools without oxidizing, exits mirror-bright, and skips the pickle-and-passivate cycle entirely.
The passive layer forms naturally in the furnace and stays intact — no acid touches it after annealing. Everything the finish is worth follows from that.
| Aspect | Standard annealed (pickled) | Bright annealed (BA) | What it decides |
|---|---|---|---|
| Furnace atmosphere | Air / combustion gases | Hydrogen or inert / vacuum | Whether scale can form at all |
| Surface after anneal | Oxide scale; pickled matte finish | Bright, scale-free, no pickling needed | Whether an acid step touches the surface |
| Oxide / passive layer | Stripped by pickling, re-passivated | Intact, formed in the furnace | Pitting initiation at the same nominal grade |
| Typical ID Ra | ~0.9–1.4 µm | ~0.04–0.6 µm depending on grade | Ferrule bite consistency and cleanability |
| Cleanliness | Pickling residue risk | No acid residues | Whether an analyzer line sees contamination |
| Cost | Lower | Higher | Where standard annealed stays the right buy |
| Typical service | General hydraulics, utilities | Instrumentation, high-purity, corrosive duty | Which of the two the line should get |
The smoother surface is not cosmetic. Bacteria and particles shelter in surface valleys — the reason hygienic and high-purity systems cap roughness — and pitting corrosion initiates at damaged passive films.
BA’s intact, enriched passive layer resists pitting initiation better than a pickled surface at the same nominal grade. In chloride-bearing instrument service that difference is the reason for the order, not a bonus.
Why does instrumentation specify it?
Three engineering reasons, and one shop-floor constraint that follows from them.
Sealing. Compression fittings bite and seal on the tube OD. A smooth, consistent, clean surface takes an even swage; rough or residue-bearing tube bites inconsistently, and inconsistent bites are the leaks that appear months later.
Cleanliness. No pickle residues and no scale inclusions: the tube arrives chemically quiet, which analyzer, pharma and semiconductor lines demand.
Corrosion. The undisturbed passive layer starts life stronger in chloride and marine environments than a pickled surface at the same nominal grade.
Consistent hardness matters too. Instrument BA tube is controlled soft enough to accept the ferrule bite — manufacturers hold it under roughly 90 HRB — which ties directly to the hardness rule in our compression fitting guides.
What goes wrong when the finish is not stated?
Most BA problems are not about the anneal. They are about a purchase order that named a standard and left the roughness inside it.
| Symptom | Most likely cause | What to change |
|---|---|---|
| Joint weeps months after assembly, tube OD looks clean | Inconsistent swage on a rough or residue-bearing OD | Put the finish and its Ra on the order, not just “A269 BA” |
| Particles or staining downstream of a new run | Pickle residue or scale inclusion from standard annealed tube | Specify BA for that line — it arrives with no acid residues |
| Pitting starts at scattered sites on a pickled line in chloride service | Passive film damaged by pickling and only partly rebuilt | Specify BA, whose furnace-formed layer is intact |
| Two BA deliveries, one measurably rougher than the other | A269 requires only a workmanlike finish and no Ra value | State the finish explicitly, for example ID Ra ≤ 0.4 µm |
| Ferrule will not take an even bite, joint feels hard to swage | Tube harder than the fitting expects | Confirm the tube is annealed BA, held under roughly 90 HRB |
Read the symptom before changing the supplier or the grade. A weeping joint, a contaminated line and a pitted surface are three different finish failures, and each one is fixed on the order rather than in the plant.
How do I write it on the purchase order?
ASTM A269 is the usual standard for seamless and welded instrument tubing, but it requires only a “workmanlike finish” and does not mandate Ra values.
Two suppliers can both ship compliant “A269 BA tube” at 0.4 and 0.8 µm — a two-fold difference that matters to a high-purity system. Five steps close that gap:
- State the service. Instrument air, analyzer sample, pharma contact or UHP gas — the service sets the finish, so it goes on the enquiry before the standard number.
- Write the finish and the Ra together. “Bright annealed, ID Ra ≤ 0.4 µm” closes the hole; a finish word with no number leaves it open.
- Name the standard and its limit. ASTM A269 with the Ra stated on the order, or ASTM A270 where surface finish is defined by grade.
- Give OD and wall. Tube and fittings quote as one system, and the ferrule has to match the OD it bites.
- Check the delivery against the finish line. An A269 certificate confirms the standard; only the stated Ra confirms the surface.
The order is complete when all of the following can be read off it without a phone call:
- Finish written as bright annealed, not inferred from “A269 BA”
- Ra value stated on the ID
- Standard named — A269 with the Ra, or A270 by grade
- OD and wall given for the tube
- Grade named in 304, 316 or 316L
- Service described in one line
FerruleX supplies BA and precision stainless tubing alongside the instrumentation tubing range and matching compression fittings — including BA tube in 304/316/316L.
Send the standard (A269 with a stated Ra, or A270), the OD and wall, and the service, and we quote tube and fittings as one system. Request a factory quote.
FAQ
What does “bright annealed” actually mean? The final heat treatment runs in a closed furnace under hydrogen or inert gas, so the tube cannot oxidize. It exits bright and scale-free with no pickling, unlike standard annealed tube, which scales in air and is acid-pickled.
Why is BA tubing better for instrumentation? A smooth, clean surface gives compression ferrules a consistent bite and seal. There are no pickling residues to contaminate analyzer or high-purity lines, and the undisturbed passive layer resists pitting initiation in chloride service.
What Ra should I specify for BA tubing? General instrumentation around Ra ≤ 0.6 µm, pharmaceutical and food contact ≤ 0.4 µm, semiconductor and UHP gas service ≤ 0.25 µm. ASTM A269 does not mandate Ra, so state the value on the order.
Is BA tubing softer than standard tube? It is annealed to a controlled softness — manufacturers hold instrument BA tube under roughly 90 HRB — so it accepts the ferrule bite. Hard tube refuses the swage.
When is standard annealed tube fine? General hydraulics and plant utilities, where surface cleanliness and corrosion initiation are not the governing concerns. It costs less and performs the same there — buy BA where the surface is doing engineering work.