Chloride stress corrosion cracking is the failure mode that takes down 316 stainless without rust, without warning and without forgiveness.
The quick answer: if a 316 line carries chlorides, sits under tensile stress and holds a metal temperature around 50–60 °C or above, the alloy decision belongs on the RFQ, not in the maintenance log. 316L does not change that answer.
A fitting that passes PMI, passes hydrotest and looks perfect can still part along a crack that grew in weeks. Cracking needs no visible corrosion to proceed — it needs chlorides, tensile stress and temperature.
The buyer’s defence is knowing the threshold band, knowing what 316L does not fix, and writing the environment on the RFQ. Then the alloy decision is made before the first failure instead of after.
Key takeaways
- Chloride SCC of austenitics is transgranular — the crack runs through the grains, not along them, and propagates fast once started.
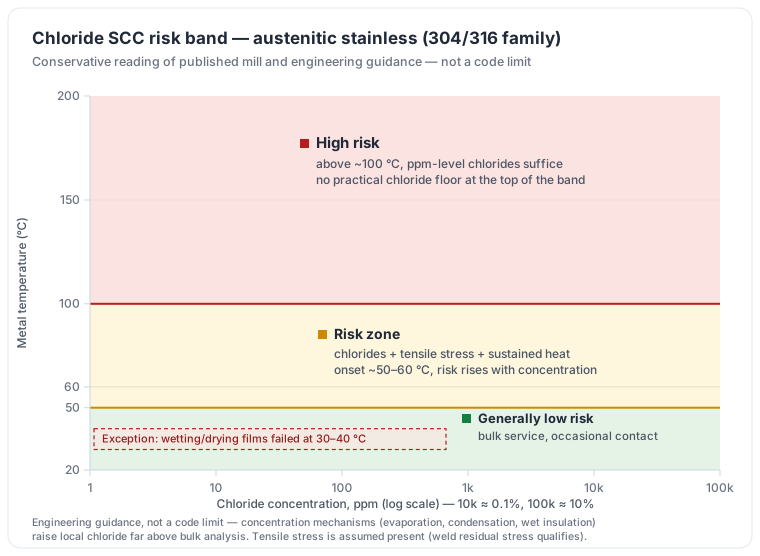
- Engineering guidance puts the risk zone at roughly 50–60 °C and up when chlorides and tensile stress coexist; above about 100 °C, ppm-level chlorides are enough.
- The stress can be residual — an untreated weld’s residual stress alone can exceed the threshold.
- 316L buys nothing here: lower carbon fixes weld sensitization, a different failure; chloride SCC tracks nickel content.
- The upgrade ladder: duplex 2205 for moderate chloride heat, nickel alloys for the hot chloride frontier, copper alloys where ammonia is absent — plus stress relief, drainage and washing as design-level defenses.
Do you actually have all three conditions?
Chloride SCC needs three conditions to coincide: chlorides, tensile stress and temperature. All three are common in plant, which is why the failure keeps appearing on lines nobody flagged. Chlorides arrive from seawater, brackish water, chloride-bearing steam, insulation leachate or condensed chlorinated atmospheres.
Tensile stress arrives from applied system pressure — or from residual stress locked around a weld that was never heat-treated. Mill data warns that untreated weld residual stress alone can approach the material’s proof strength.
Temperature is the accelerator. Where pitting is visible and slow, chloride SCC is invisible and fast. The crack path is transgranular, running through the grains under combined chemical-mechanical attack. A crack can penetrate a wall before any surface sign appears.
Where the three conditions meet:
- Coastal and marine atmospheres — salt aerosol on warm equipment.
- Seawater and brackish service.
- Chloride-bearing steam and condensate.
- Insulated lines where moisture wicks chlorides against the metal — CUI.
- Building services — the pool-hall cases showed 316 ducting and supports cracking at 30–40 °C under chloramine-laden condensation.
The through-line is concentration. Any geometry that lets a thin chloride film sit and dry repeatedly is a candidate, whatever the bulk analysis says.
Score the three. Two present is a design review. All three present is an alloy conversation.
What temperature and chloride level actually matter?
No single number exists. The published guidance is a band, and the honest way to draw it is conservative:
| Temperature band | Engineering guidance | What it decides |
|---|---|---|
| Below ~50 °C | Generally low risk for 304/316 in occasional chloride contact — but repeated wetting-drying films have failed at 30–40 °C. Mill datasheets; documented pool-hall cases | Whether a cool line can be called safe — only if the film never concentrates and dries |
| ~50–60 °C and up | Risk zone begins: chlorides, tensile stress and sustained temperature together. Alleima, Outokumpu and EEMUA 194 guidance | Whether the alloy question moves onto the RFQ |
| Above ~100 °C | Chlorides in the ppm range suffice. Mill datasheet wording, verbatim | Whether bulk ppm chemistry can rule the risk out — at this temperature it cannot |
Treat this table as engineering guidance, not code. The industry rules themselves say the limit is subject to debate, and concentration mechanisms are the wild card. Evaporation, condensation and insulation-leached chlorides concentrate locally far above the bulk chemistry.
Corrosion-under-insulation references put the susceptible skin-temperature window for austenitics under wet insulation at roughly 50–175 °C. That is exactly where a lot of outdoor 316 pipe lives.
The same band as a picture — the conservative zones, with the wetting-drying exception sitting below the line and no practical chloride floor at the top:
Why does 316 crack without warning?
The most famous demonstration is the 1985 Uster swimming-pool roof collapse. Stainless tension rods cracked by chloride SCC in a warm, chlorinated atmosphere, at temperatures well below the classic thresholds.
That case is the warning: the damage looked like nothing until the structure let go. The table below reads from what an inspector finds back to what has to change.
| Symptom | Most likely cause | What to change |
|---|---|---|
| Crack through the wall, no rust or thinning beside it | Transgranular chloride SCC under sustained tensile stress | Change the alloy — surface condition is not the variable here |
| Crack at or beside a weld that was never heat-treated | Weld residual stress alone, at or above the threshold | Stress-relieve or shot-peen, and re-run the alloy decision |
| Failure under wet insulation on a warm line | Chloride concentration inside the ~50–175 °C CUI skin-temperature window | Keep insulation dry and clad it, then review the alloy for the real skin temperature |
| Failure at 30–40 °C in a pool hall | Chloramine-laden condensation and repeated wetting-drying films | Treat wetting-drying as a risk condition, not as a cool-line exemption |
| Pits or crevices with a crack starting from them | Pitting acting as the initiation site for cracking | PREN scores pitting only — the SCC decision still needs the three conditions |
Pits and crevices are cousins of the crack, not a different problem. The pitting side of chloride behaviour is covered in pitting corrosion in stainless steel fittings, and the weld-zone half of the story in passivation of stainless steel fittings.
Which alloy do you move to?
316L is not an answer. The L grade caps carbon at 0.03% to stop weld-zone carbide precipitation — intergranular corrosion, a different failure. Chloride SCC tracks nickel. Austenitics at 8–12% Ni sit in the vulnerable band, and mill guidance puts good practical resistance at about 25% nickel. Alloy 20 and 904L earn their keep here.
| Route | Where it stands in chloride service | What actually decides it |
|---|---|---|
| 316 and 316L | Same vulnerable band at 8–12% Ni; the L suffix fixes weld sensitization, not cracking | Whether chlorides, stress and temperature are genuinely all present |
| Duplex 2205 | Markedly more resistant than 316 — mixed microstructure and higher strength raise the threshold — but not immune | Moderate chloride heat, without hot concentrated chlorides |
| Alloy 20 / 904L, ~25% Ni guidance | Practical resistance at about 25% nickel | Nickel content, not the L suffix |
| Nickel alloy 625 | Effectively immune in practical chloride service, at a price | The hot chloride frontier, where the cost is defended |
| Copper alloys | Ignore chloride SCC entirely | Ammonia must be absent — brasses crack in ammonia |
| Free defences — stress relief, shot peening, crevice design, washing, dry insulation | Lower the stress and the concentration without changing alloy | The residual stress and the geometry you can actually change |
“More resistant” is not immune. Duplex has its own limits in hot concentrated chlorides, and nickel alloys carry the price that reserves them for the frontier.
Which is why the upgrade decision belongs on the RFQ, with the environment stated — not as a blanket surcharge on every line, the way oversized valves waste money in valve sizing gone wrong.
And the free defences are still yours: stress-relieve or shot-peen where possible, design crevices and dead pockets out, keep surfaces washed, and never let insulation sit wet on hot stainless.
How do you check a line before you order?
- Write the medium and its chloride source. Bulk ppm, plus any concentration mechanism you know of — condensation, evaporation or insulation leachate.
- Take the metal temperature, normal and upset. Metal temperature, not fluid temperature; the risk band starts around 50–60 °C.
- Mark every weld and every crevice. They are the default stress source and the default crack initiation site.
- Hunt the concentration mechanism. Wet insulation, wetting-drying films, dead pockets that let a chloride film sit and dry.
- Score the three conditions. Two present is a design review; all three present is an alloy conversation — duplex first, nickel alloy at the frontier.
What goes on the RFQ?
Four lines, written on the enquiry:
media and chloride content— bulk ppm, plus any concentration mechanism known.temperature band— normal and upset, metal temperature not just fluid.welded construction?— HAZ residual stress is the default stress source.environment— coastal, insulated, pool-adjacent, steam-adjacent: words that change the alloy shortlist.
Send those four with the size list and the alloy question is settled before quoting starts. Request a factory quote.
FAQ
Does 316L resist SCC better than 316?
No. The L grade caps carbon at 0.03% to stop weld-zone carbide precipitation — intergranular corrosion, a different failure. Chloride SCC tracks nickel, so 316 and 316L sit in the same band.
At what temperature does chloride SCC start in 316?
Engineering guidance puts risk onset at roughly 50–60 °C when chlorides and tensile stress coexist; above about 100 °C, ppm-level chlorides suffice. Concentrated wetting-drying films have failed at 30–40 °C.
Is duplex stainless immune to chloride SCC?
No. Duplex 2205 is markedly more resistant than 316 — higher strength, mixed microstructure — and extends the service window substantially. In hot concentrated chlorides it still has limits, so hostile heat goes to a nickel alloy.
How do I know if my application is at risk?
Three questions: chlorides in the medium or environment; sustained metal temperature above ~50 °C or a mechanism that dries films on the metal; tensile stress, which welded construction already gives you. All three mean an alloy conversation.
What is the difference between chloride SCC and pitting?
Pitting is visible local attack from chloride breakdown of the passive film, measured by PREN. SCC is cracking from chlorides, tensile stress and temperature, with almost no visible corrosion. Pits often initiate cracks, and PREN does not score SCC.