Passivation is the acid treatment that removes free iron and other contaminants from the surface of stainless steel so the chromium-rich passive film can form cleanly — it restores the surface’s own corrosion resistance rather than adding any coating.
It is a cleaning-and-restoration step, not a coating. Machined parts need passivation; welded parts need pickling first and passivation after. Passivation cannot remove weld tint, heal pits, or change the alloy.
Every machined fitting arrives from the shop with embedded iron and shop contamination on its surface. Passivation is the step that turns freshly machined stainless back into corrosion-resistant stainless.
Key takeaways
- Passivation removes free iron and shop contamination and lets the chromium oxide passive film form evenly — it is a cleaning-and-restoration step, not a coating and not a repair.
- Nitric acid immersion is the traditional method; citric acid is the lower-hazard alternative accepted under ASTM A967 — both need clean parts, controlled time and temperature, and thorough rinsing.
- Weld heat tint is not passivation territory: removing the chromium-depleted oxide layer from welds is pickling, a stronger acid treatment, often with paste for local work.
- Passivation will not remove pits, will not fix rust bloom from contamination sitting in service, and will not rescue a wrong-grade selection — those need rework, cleaning, or a different grade.
Which process do I need?
The choice follows the condition of the part, not the alloy. Machined and clean parts take passivation; anything carrying weld tint takes pickling first. The decisive column below is the one that settles most enquiries.
| Method | What it removes | Use it when | What decides it |
|---|---|---|---|
| Nitric acid immersion | Free iron and light contamination; oxidizing conditions promote the passive film | Production batches of machined fittings and valves | The hazard controls you have — fume control, PPE, waste handling — and a rinse verified neutral at the end |
| Citric acid immersion | Free iron via chelation; supports film formation | The same duty with lower hazard and easier disposal | Milder chemistry: time, temperature and concentration must be validated per A967 for the alloy |
| Pickling (immersion or paste) | Weld heat tint, oxide scale and the chromium-depleted layer beneath | Weldments, welded tube systems, locally heat-tinted zones | Whether tint is present — if it is, passivation alone will not remove it |
The pickling row is the one buyers confuse most often. Weld tint is a chromium-depleted oxide skin with reduced corrosion resistance, and passivation alone does not remove it. Welded assemblies therefore need pickling first and passivation after.
The same distinction decides what to ask for after fabrication: passivated fittings for machined parts, pickled-and-passivated for welded ones. For hygienic duty the documentation habit is the same as sanitary stainless fittings describe, and the food-plant context for it sits on the food & beverage page.
How does passivation work?
Stainless steel protects itself with a passive film of chromium oxide a few atoms thick, and that film forms spontaneously when a clean surface meets oxygen.
Machining, cutting and handling smear free iron and shop grime across the surface. That iron rusts first, stains the part, and seeds pitting under the film. Passivation dissolves it without attacking the bulk stainless, so the film forms clean and continuous once the part is rinsed and exposed to air.
The standards frame it. ASTM A967 covers chemical passivation treatments for stainless steel parts, and ASTM A380 is the broader practice for cleaning, descaling and passivating parts and systems.
A point both make that buyers miss: a visibly clean surface is the prerequisite. Passivation is not degreasing, and acids do not remove oil or scale.
How do I run it in the shop?
Five steps, and each one depends on the one before it. Skip the clean stage and the acid bath does nothing for the contamination still sitting on the metal.
- Clean before acid. Remove oil, grease and scale first. Passivation is not degreasing, and an acid does not shift oil.
- Pickle where there is weld tint. Weld heat tint is a chromium-depleted oxide layer, and passivation alone does not remove it.
- Apply the acid treatment. Nitric or citric immersion per ASTM A967, at the time, temperature and concentration of the qualified procedure for that alloy.
- Rinse thoroughly. Verify rinse neutrality before the part dries — rinsing is part of the treatment, not a formality after it.
- Let the film form, then protect it. Rinse and air exposure re-form the chromium oxide film. Handling and packing decide whether it survives the container.
Why does stainless still rust after welding?
Rust blooming near welds has three usual causes, and each has its own fix. The table maps the symptom you see to the cause that most often produces it.
| Symptom | Most likely cause | What to change |
|---|---|---|
| Rust bloom beside a weld | Weld heat tint — a chromium-depleted oxide layer that rusts unless removed | Pickle the tint, then passivate the part |
| Rust speckling away from welds | Embedded iron from carbon-steel brushes, grinding dust or steel wool dragged across the surface | Clean the contamination, re-passivate, and change tooling discipline |
| Local staining where chlorides settle | Chlorides concentrating on a roughened weld zone until the film breaks down | Control the environment, or change grade |
| Pitting that survives treatment | Metal already lost to pits | Qualified rework or replacement |
| Freshly treated parts stained again | Carbon-steel swarf or contaminated packing inside the container | Fix handling and packing, not the acid |
A final passivation after fabrication restores the film across the whole part. Hold the distinction: a machined fitting that arrives stained from the shop is a cleaning problem, while a fitting that rusts in chloride service after installation is a design or grade problem.
The pitting side of that story is covered in pitting corrosion.
What can passivation not fix?
The limits matter because they decide whether passivation is the answer or the wrong tool.
- It does not repair pits. Metal already lost stays lost, and the honest options are qualified rework or replacement.
- It does not remove heat tint, scale or heavy oxides. That is pickling.
- It does not change the alloy. A 304 fitting passivated for chloride duty is still a 304 fitting, and the right answer is 316 or duplex, not a stronger acid.
- It is not a licence to skip handling discipline. Passivated parts shipped in a container with carbon-steel swarf arrive contaminated again.
What should I put on the RFQ?
Name the requirement rather than assuming it is standard. A supplier quoting blind will guess the process, and the paperwork will not match it.
- The standard: passivation per ASTM A967 after machining.
- The method, if you have one: nitric or citric.
- The treatment for welded parts: pickle plus passivate.
- Which items are machined only and which are welded.
- The documentation you expect with the shipment.
- Whether hygienic duty applies, so the records match that duty.
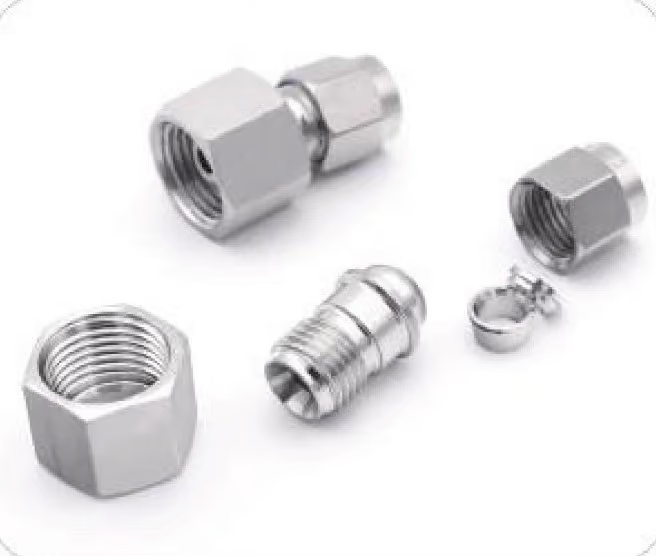
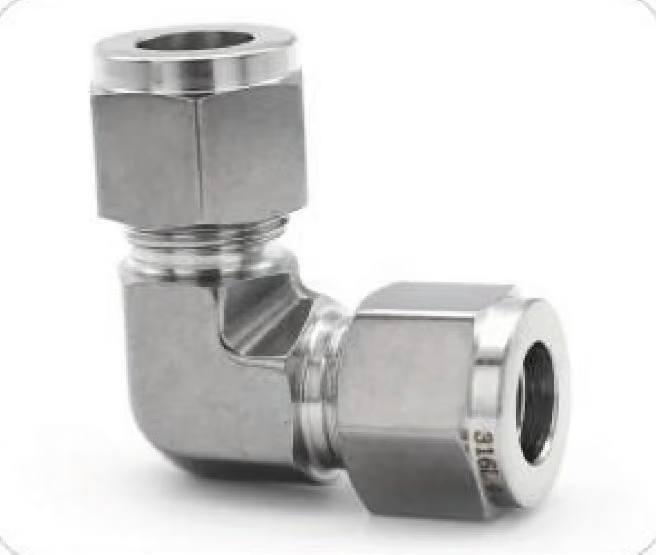
FerruleX supplies machined cast fittings and compression bodies in passivated condition. Welded assemblies can be pickle-and-passivated to order.
State the standard and the documentation you need on the RFQ, then request a factory quote.
FAQ
Why does stainless steel rust after welding? Weld heat tint rusts because it is a chromium-depleted oxide layer; embedded iron from carbon-steel tools and grinding dust rusts; chlorides concentrate on the roughened weld zone. Fixes: pickle, clean, or change environment and grade.
How do you prevent stainless steel from rusting? Choose the grade for the chloride level — 316 where chlorides are real, duplex for severe service — and passivate after fabrication. Keep chlorides and deposits off the surface, eliminate crevices, and do not let washdown chemistry dry on fittings.
What is the difference between passivation and pickling? Passivation removes free iron and light contamination and lets the passive film form with nitric or citric acid. Pickling is stronger — typically nitric-hydrofluoric — and removes weld tint, scale and the chromium-depleted layer. Welded parts need pickling first, then passivation.
Will passivation remove or stop pitting? No on both counts. It cannot replace metal already lost to pits, and it cannot make a pitted or crevice-ridden environment benign. Pits need qualified rework or replacement; the environment needs design or maintenance change.
What should I specify on the RFQ for passivated fittings? Name the standard — passivation per ASTM A967 after machining — the method if you have one, nitric or citric, and the treatment for welded parts: pickle plus passivate. Ask for certificates with the order.