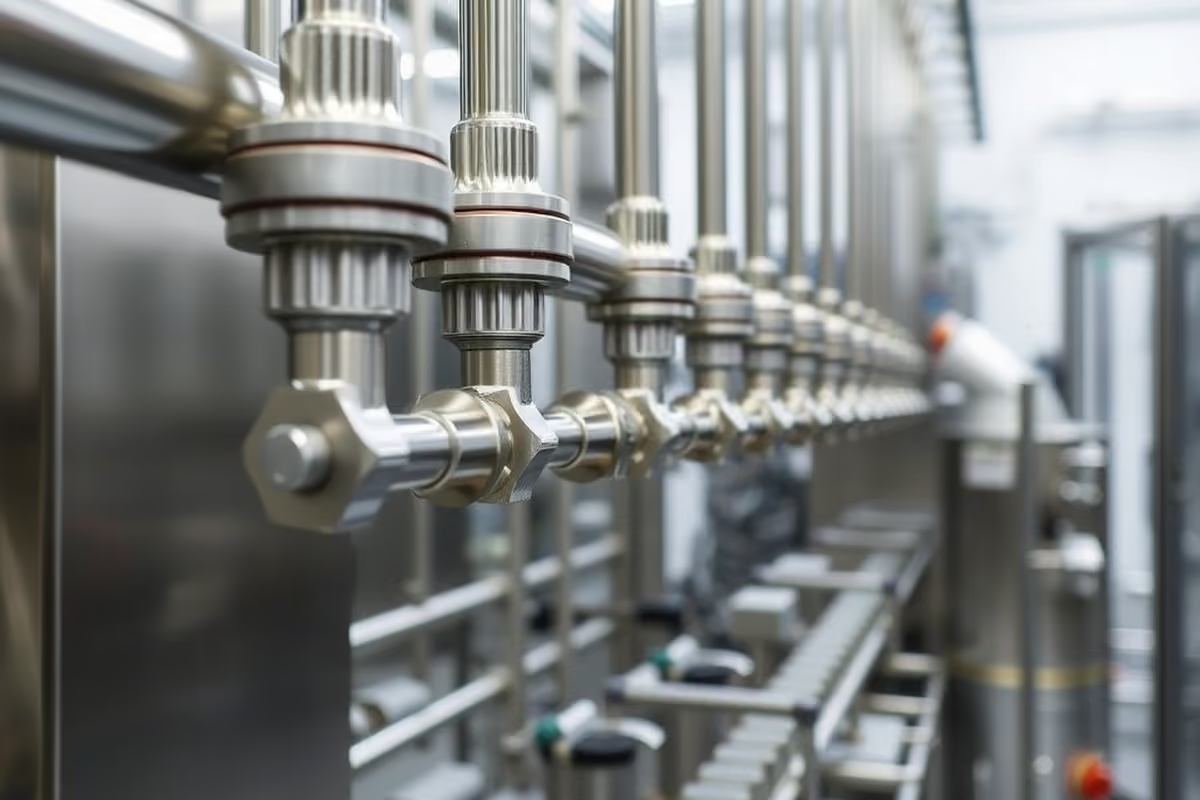
“Sanitary” is not a marketing adjective — it is a set of measurable requirements, and sanitary stainless fittings differ from industrial ones in ways an auditor can verify with a surface gauge and a flashlight. If your line carries food, dairy, beverage or pharma product, the differences decide whether your CIP cycle actually cleans the pipe or just rinses it.
Key takeaways
- The sanitary defaults are 316L (for welded chloride service), a controlled product-contact surface finish — commonly 20 µin Ra (≈0.5 µm) mechanical polish for food duty, 15 µin (≈0.38 µm) electropolish for pharma and high-purity water — and a crevice-free, fully drainable geometry.
- The frameworks do different jobs: 3-A Sanitary Standards cover food, dairy and beverage equipment design; ASME BPE governs bioprocess and pharmaceutical piping with stricter finishes and traceability; EHEDG publishes European hygienic design guidance, with cleanability validated to about Ra 0.8 µm.
- Dead legs, crevices and threaded connections are the audit killers: keep branch dead legs within roughly three pipe diameters, avoid thread and gasket crevices on product contact, and standard industrial fittings upstream of the process boundary are fine.
What “food-grade” actually specifies
Four things separate a sanitary fitting from its industrial cousin, and each is checkable:
| Aspect | Industrial standard | Sanitary / food-grade requirement |
|---|---|---|
| Material | SS304 or SS316 by cost and corrosion | SS316L default, especially for welded lines (weld decay — see SS304 vs SS316) |
| Surface finish (ID) | Mill finish or unspecified | Controlled Ra: ~20 µin (0.5 µm) mechanical polish food-grade; 15 µin (0.38 µm) electropolish pharma/WFI |
| Geometry | Any that holds pressure | Crevice-free, self-draining, no thread contact with product; dead legs ≤ ~3 pipe diameters |
| Documentation | Mill cert on request | Heat traceability, finish certification, 3-A symbol or BPE compliance where specified |
The surface number matters because of what lives in the valleys: above roughly Ra 0.8 µm, bacteria shelter from CIP flow in the surface texture, which is why hygienic standards sit well below that threshold — and why a “smooth looking” mill finish fails.
The three frameworks, and which one applies
3-A Sanitary Standards are the food, dairy and beverage framework: they name acceptable alloys, product-contact surface finishes, listed elastomers, and design rules for drainability and crevice-free internals. If your customer is a dairy or beverage plant, 3-A is the language the auditor speaks.
ASME BPE (Bioprocessing Equipment) is the pharmaceutical and bioprocess standard — stricter in finishes, welding quality and traceability. Its product-contact surface series runs SF1 through SF6: SF1 is the 20 µin mechanical polish that usually suffices for food-grade work, while SF4 — the same roughness ceiling achieved with electropolishing — is the usual callout for purified water, WFI and biological product contact.
EHEDG is the European hygienic design authority; its cleanability testing underpins the Ra thresholds above and its guidance covers layout and equipment design rather than certifying individual fittings. On export projects, expect European buyers to reference EHEDG logic and American buyers to reference 3-A — the engineering underneath is compatible.
Pick the framework before the fitting, because it sets the finish, the paperwork and the vocabulary the auditor uses:
| Framework | What it governs | The question that decides it |
|---|---|---|
| 3-A Sanitary Standards | Food, dairy and beverage equipment design: acceptable alloys, product-contact finishes, listed elastomers, drainability rules | Is the receiving plant a food, dairy or beverage operation? Then 3-A is what its auditor reads. |
| ASME BPE | Bioprocess and pharmaceutical piping: finishes, weld quality, traceability, the SF1–SF6 product-contact series | Is the product biological, WFI or purified water? Then BPE, and usually SF4 electropolish. |
| EHEDG | European hygienic design guidance — layout and equipment, cleanability validated to about Ra 0.8 µm | Is the buyer European and asking for cleanability logic rather than a symbol on a fitting? |
Where standard industrial fittings are fine
Not every fitting on a food plant needs the sanitary treatment. Utility lines — compressed air, cooling water, CIP supply headers upstream of the process boundary, drain and vent plumbing — carry no product and face no audit of product-contact surfaces.
Standard threaded compression fittings and valves are cheaper, stocked deeper, and perfectly appropriate there. The discipline is the boundary: mark where product contact begins, and hold that line in the BOM, because an auditor will.
Set the boundary item by item — the last column is the one that decides:
| Line or item | What to fit | The question that decides it |
|---|---|---|
| Product-contact run — food, dairy, beverage | Sanitary pattern, 316L, controlled Ra, 3-A where the buyer requires the symbol | Does product or CIP return flow through it? |
| Product-contact run — pharma, bioprocess, WFI | ASME BPE, SF4 electropolish at 15 µin (≈0.38 µm), heat traceability | Is the fluid a biological product or purified water? |
| CIP supply header upstream of the process boundary | Standard threaded compression, no finish callout | Does it carry product, or only cleaning solution up to the boundary? |
| Compressed air, cooling water | Standard industrial, mill finish acceptable | Is there any product contact at all? |
| Drain and vent plumbing | Standard industrial | Is there any product contact at all? |
Gaskets and CIP/SIP reality
Sanitary joints live on elastomer gaskets, and the gasket is as much a spec as the fitting: EPDM for steam and hot CIP, PTFE for aggressive chemistry, FKM where oils and solvents appear — the same logic as tri-clamp gasket selection covers in detail.
Every gasketed joint is also a crevice by definition, which is why clamped sanitary connections are designed to be broken, inspected and rebuilt on a schedule. Design the line for CIP velocity and drainage — a fitting that traps product defeats a perfect surface finish.
What fails an audit, and what fixes it?
Every finding below has a physical cause, and most are one line item away from being fixed:
| Symptom | Most likely cause | What to change |
|---|---|---|
| CIP runs to schedule, rinse water still carries product | A dead leg or a gasket crevice holding soil out of the flow | Bring the branch within roughly three pipe diameters; break, inspect and rebuild the joint |
| Counts climb again a few cycles after CIP | Surface too rough — above roughly Ra 0.8 µm the texture shelters bacteria from CIP flow | Specify a controlled finish: 20 µin (≈0.5 µm) mechanical, 15 µin (≈0.38 µm) electropolish |
| Auditor writes up a joint on product contact | Thread crevices on the wetted path | Move that joint to a clamp or weld end; keep threads on utility lines |
| Localised attack along a weld on a 316 line | Weld decay — why 316L is the sanitary default | Respec the alloy to 316L |
| Finish certificate rejected on delivery | No Ra number, no standard, no heat traceability on the line item | Write Ra, 3-A or ASME BPE, and traceability into the BOM |
| Product stands in a branch after draining | Branch beyond roughly three pipe diameters, or a joint that does not self-drain | Shorten the branch; specify self-draining geometry |
| Gasket swells or hardens | Elastomer not matched to the duty | EPDM for steam and hot CIP, PTFE for aggressive chemistry, FKM for oils and solvents |
What goes on the line item?
Seven calls, in this order — each one narrows the next:
- Boundary. Mark where product contact starts. Everything above it stays industrial; nothing below it does.
- Alloy. 316L as the default, especially for welded and chloride duty; 304 only for non-wetted utility service.
- Surface. 20 µin (≈0.5 µm) mechanical polish — ASME BPE SF1 — for food, dairy and beverage. 15 µin (≈0.38 µm) electropolish — SF4 — for pharma, WFI and biological contact.
- Geometry. Crevice-free and self-draining, no thread on product contact, branch dead legs within roughly three pipe diameters.
- Connection. Tri-clamp where the joint must break down for inspection without tools; weld ends or specialty dairy connections where the run is permanent, finished and qualified to the same standard.
- Gasket. A spec, not an accessory: EPDM for steam and hot CIP, PTFE for aggressive chemistry, FKM for oils and solvents.
- Documentation. Name 3-A or ASME BPE, and require with the delivery:
- heat traceability for the heat number on the fitting,
- finish certification for the Ra called out,
- the 3-A symbol or BPE compliance statement where the standard requires it,
- the listed elastomer identified on the gasket.
FerruleX manufactures sanitary-pattern cast fittings and tri-clamp-end assemblies — browse the cast fittings category or the tri-clamp corrugated hose style, and send the standard (3-A or BPE), finish, alloy and sizes with your RFQ. For clamp sizing, what are tri-clamp fittings has the measurement rules. Request a factory quote.
FAQ
What makes a fitting “sanitary” or food-grade? A controlled product-contact finish — roughly 20 µin Ra for food duty, 15 µin electropolish for pharma — an approved alloy such as 316L, crevice-free self-draining geometry, and documented 3-A or ASME BPE compliance.
Is 316 required for food-grade fittings? 316L is the sanitary default, especially for welded lines — low carbon prevents weld decay. 304 may suit non-wetted utility fittings or mild, non-chloride duty. On spec-sensitive food and pharma lines, deviation should be documented, not silent.
What Ra finish do I need? Food, dairy and beverage duty takes a 20 µin (≈0.5 µm) mechanical polish, ASME BPE SF1. Pharma, WFI and biological contact takes 15 µin (≈0.38 µm) electropolish, SF4. Conversions and the SF0–SF6 designations are on the Ra surface finish chart.
Do sanitary fittings have to be tri-clamp? No — weld ends and specialty dairy connections are equally sanitary when properly finished and qualified. Tri-clamp is dominant because it breaks down for inspection without tools; whatever the connection, the requirements are the same: crevice-free, drainable, cleanable, documented.
Where do industrial fittings fail an audit? On product contact: threaded joints that harbor product, unspecified finishes that shelter bacteria, dead legs beyond a few pipe diameters, unlisted elastomers, no traceability. Each is a written finding, and each was cheap to avoid at specification time.