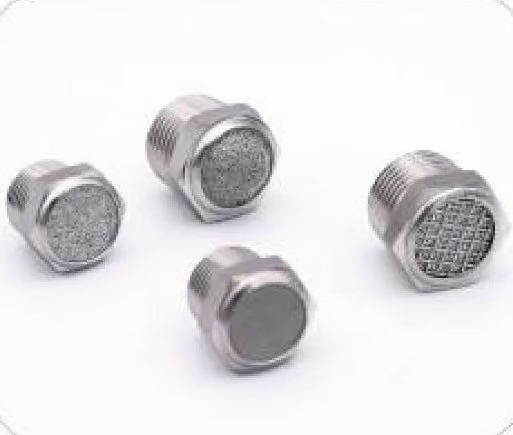
Gauge snubbers are the cheapest insurance in the instrument rack — a small threaded restriction that sits between the process and a pressure gauge and stops the pointer from being hammered to death.
Fit one wherever the gauge sees a reciprocating pump, a compressor or fast valve actuation. The construction follows how dirty the fluid is; the orifice grade follows viscosity. It passes steady pressure, averages rapid change, and cannot isolate.
Key takeaways
- Pulsation and vibration are leading gauge killers — pointer flutter is the symptom, fatigue of the sensing element is the bill.
- A snubber is a restriction the process fluid must squeeze through: it passes steady pressure and averages out rapid change; it does not change the process pressure.
- Three working types: fixed drilled orifice, porous sintered disc, and piston (self-cleaning, sometimes adjustable with a needle).
- Sizing follows the fluid: finer restriction for gases, coarser for viscous liquids — and over-damping hides real pressure changes.
- A snubber is not an isolation valve: the loop needs both, snubber for damping plus a gauge root valve for service.
Which snubber do I need?
The choice turns on dirt and on how predictable the pulsation is — not on pressure class, which the panel fixes anyway. Three constructions cover the market, plus an adjustable variant of the piston:
| Type | How it dams | Service it suits | What actually decides |
|---|---|---|---|
| Fixed drilled orifice | A disc with a precision hole; the hole is the restriction | Clean, predictable service | Dirt — the hole clogs in dirty service, and clean service is what makes it the simplest and cheapest part |
| Porous sintered disc | Fluid percolates through a porous element that averages pulsation across its whole surface | Moderate dirt | How much dirt the element can swallow before it blinds |
| Piston | A floating piston seats against the orifice on a sudden pressure rise and meters the flow | Dirty or variable service | Whether the pulsation character is known before start-up |
| Piston, adjustable | The same piston with a needle added for on-site tuning | Commissioning an unknown duty | Whether you can watch the needle and tune it |
Typical construction is 316 stainless in 1/4 or 1/2 NPT, with common sizes in the 6,000 psi class. Bigger ratings exist, but for most instrument panels that is the working range.
The part list is short by design: body, seal, restriction. A snubber that costs less than the gauge’s shipping crate can double the gauge’s life.
That is what makes it a fleet item — stock one per gauge size class and the next pulsation problem is an afternoon fix, not a purchase order.
What is killing the gauge?
Failure reports read the same way everywhere: excessive pulsation and vibration at the top. Gauge data sheets concede the pattern — most field failures trace to dynamic abuse, not to defective instruments.
| Symptom | Most likely cause | What to change |
|---|---|---|
| Black powder inside the case, movement stiff or worn | High-frequency vibration grinding the movement’s gear teeth | Damp at the gauge; check the mounting and the pulsation source |
| Pointer flutter that never settles | Low-frequency pulsation flexing the Bourdon tube thousands of cycles per shift | Fit a snubber graded to the fluid — element fatigue is the bill |
| Dented pointer, deformed or ruptured tube | Water-hammer spike from fast valve closure or pump switching | Fix the transient at source: closure rates, surge suppression, instrument range |
| Gauge reads wrong after an event but is not broken | Overpressure degrading accuracy | Range selection or a relief device; damping will not help |
Only the first two rows are the snubber’s job. A water-hammer transient and a true overpressure event are system and range problems, and no restriction in the gauge line fixes either.
Loop-level defences are covered in instrument manifolds, and the check-valve selection logic in types of stainless check valves. The snubber is the point defence for the gauge itself.
How does a restriction damp pulsation?
A snubber inserts a deliberate restriction — a small orifice the process fluid must pass through — between the process and the gauge.
Rapid pressure change is throttled by that orifice, so spikes and pulsation are averaged before they reach the element. Steady pressure, which has all the time in the world, equalizes across it.
The snubber does not alter process pressure. It changes only how fast pressure is allowed to arrive.
- Passes steady pressure unchanged — equilibrium equalizes across the restriction.
- Averages rapid change before it reaches the sensing element.
- Does not alter process pressure; it governs arrival rate only.
- Damps pulsation; it does not protect the gauge against true overpressure.
The piston variant floats a piston against the orifice: a sudden pressure rise seats it and the flow is metered through. Makers ship swappable pistons in several orifice sizes, so damping can be tuned without replacing the part, and adjustable versions add a needle for on-site tuning.
How do I size the orifice?
The trade is response against damping, and the fluid picks the starting point. The smaller the orifice, the harder the damping and the slower the reading.
Maker guidance selects the grade by viscosity: finer restriction for gases and steam, coarser for water and light oil, coarser still for viscous liquids, because viscous fluid resists the orifice on its own.
Adjustable and multi-piston snubbers exist precisely because the right hole is hard to predict from the desk. Install, watch the needle, and tune until the pointer is steady yet still follows real process change.
Step 1 — confirm the gauge is being abused. Pointer flutter or black powder in the case is dynamic abuse; a gauge that reads wrong while steady is a range or instrument problem.
Step 2 — match the thread. 1/4 NPT or 1/2 NPT, matching the gauge port.
Step 3 — pick the construction from the dirt. Fixed orifice for clean service, porous disc for moderate dirt, piston for dirty or variable service.
Step 4 — set the grade from the viscosity. Finer for gases and steam, coarser for water and light oil, coarser still for viscous liquids.
Step 5 — tune it running. Watch the needle and open the restriction until the pointer is steady and still follows normal process swings.
Two things go wrong at this stage. Over-restricting delays the reading enough to mislead operators during fast transients, and a snubber damps — it does not protect against true overpressure, which is a range-selection or relief-device problem.
Do I still need a gauge valve?
Yes — different jobs, both required. The gauge root valve is either open or closed and the process flows through it freely; the snubber is a permanent restriction the process flows through continuously. It can never isolate, and tightening a needle snubber to shutoff is not a service valve.
| Aspect | Gauge root valve | Snubber | What it decides |
|---|---|---|---|
| Job | Isolates the gauge for maintenance | Damps pulsation continuously | Two jobs, so the loop needs both |
| Normal state | Open or closed; process flows through freely | A fixed restriction; process flows through continuously | One is a service device, one is a permanent restriction |
| Can it isolate? | Yes | Never | A needle snubber tightened to shutoff is not a service valve |
| Position in the hook-up | Above the snubber, on the tapping | Below the valve, at the gauge | Isolation above, damping below |
Standard hook-up, in order:
- Process tapping on the line.
- Root valve at the tapping — isolation for maintenance.
- Snubber downstream of the valve — the damping restriction.
- Gauge last, protected by the restriction below the valve.
What do I put in the RFQ?
Five lines carry the enquiry, and the maker picks the grade from the media and pulsation lines:
thread— 1/4 NPT or 1/2 NPT, matching the gauge port.type— fixed orifice, porous disc, piston, or adjustable.media and viscosity— gas, water or oil at stated viscosity; the maker picks the grade from this.pressure class— 6,000 psi covers most panels.pulsation source— pump or compressor duty tells the factory how hard the damping needs to work.
State the response you need — pointer steady but still following normal process swings — and let the grade follow.
FAQ
Does a snubber affect accuracy?
At steady state, no — equilibrium pressure equalizes across the restriction, so the gauge reads true. What the snubber adds is response lag: real process changes take longer to show.
What is the difference between a snubber and a gauge valve?
A gauge valve isolates — open or closed, full flow, zero damping — for maintenance and calibration. A snubber damps: a restriction the process flows through continuously, averaging pulsation, with no shutoff ability. The loop needs both.
Which snubber type should I choose?
Fixed drilled orifice for clean, predictable service where cost rules. Porous disc for moderate dirt. Piston for dirty or variable service, self-cleaning with swappable orifices; take the adjustable needle version when pulsation is unknown until start-up.
Can a snubber fix water hammer?
No. It averages the high-frequency ripple a pump or compressor produces and blunts small spikes, but a water-hammer transient is a system event. Fix it at source: closure rates, surge suppression, correctly ranged instruments.
How do I size the orifice for my service?
Give the maker the media, its viscosity and the pulsation source. Catalogue practice matches grade to fluid: finer for gases and steam, coarser for liquids, coarsest for viscous service. Piston and adjustable types tune on site.