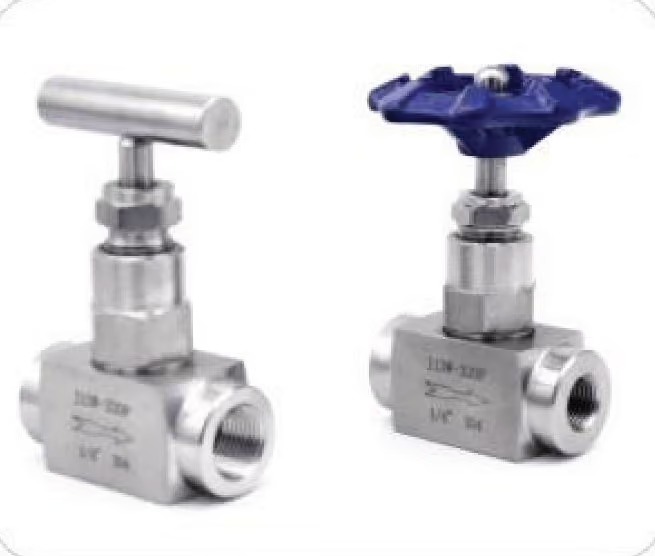
Integral bonnet is machined into the body as one piece; union bonnet threads in as a separable joint. The integral design is smaller and has fewer leak paths, while the union lets the stem assembly lift out for repacking with the body still in the line. Service access decides first and pressure class second — above 6,000 psi (414 bar) only the union family covers the duty.
Once a needle valve leaves the 3,000 psi neighborhood, its bonnet construction — the way the stem assembly seals to the body — becomes the specification that matters most. High-pressure needle valves come in two families: integral bonnet, machined from one piece, and union bonnet, a threaded separable joint. Each wins in a different corner of HP duty.
Key takeaways
- The bonnet is the stem’s pressure boundary: integral bonnets are machined into the body for compactness and economy in fixed HP service, while union bonnets join by a threaded union for repacking and trim maintenance without removing the valve from the line.
- Typical classes line up by construction: integral bonnet designs commonly run to about 6,000 psi (414 bar), while union bonnet families cover 6,000 psi standard and extend to 10,000 psi (690 bar) in high-pressure series.
- Packing picks the temperature ceiling — PTFE to about 450 °F (232 °C), graphite to 700 °F (371 °C) and beyond with high-temperature options — so the bonnet choice, pressure class and packing must be specified together, not as afterthoughts.
Which one do I need?
The bonnet carries the stem through the pressure boundary. It holds the packing that seals around the moving stem, and it anchors the stem threads.
On better designs it also provides back-seating that isolates the packing when the valve is fully open. Everything that keeps an HP valve leak-tight at the stem lives in the bonnet, which is why two constructions divide the market above utility pressures.
| Decision | Integral bonnet | Union bonnet | What actually decides it |
|---|---|---|---|
| Pressure class | To ~6,000 psi (414 bar); forged designs 5,000–6,000 psi | 6,000 psi (414 bar) standard; to 10,000 psi (690 bar) | Class above 6,000 psi leaves only one family |
| Service access | Packing via stem hardware; trim work takes the valve off | Stem and packing assembly lifts out; body stays in the line | Whether it will be repacked or retipped during its life |
| Joints and envelope | One piece, no separable joint, compact | One extra threaded joint, larger envelope | Panel density and the space the install allows |
| Cost | Lower | Higher | Budget against maintenance access |
| Duty pattern | Set once: gauge roots, calibration ports, fixed dosing lines | Opened, adjusted or repacked in service | The duty pattern, not the datasheet headline |
Read the last column first. A class above 6,000 psi (414 bar) leaves one family, and a valve that will be repacked in service repays the union’s extra joint the first time it is opened.
Why pick an integral bonnet?
An integral bonnet is machined from the same barstock or forging as the body — no separable joint at all. The virtues follow directly: fewer leak paths, a compact envelope that suits dense instrument panels, lower cost, and a body that tolerates vibration well. Forged integral designs commonly rate to roughly 5,000–6,000 psi.
The trade is maintenance. The packing is adjusted and replaced through the stem hardware, and reaching internal trim means the valve leaves the line.
For HP points that are set once and rarely touched — gauge roots, calibration ports, fixed dosing lines — the integral construction is the economical answer.
Why pay for a union bonnet?
A union bonnet screws into the body across a precision threaded joint, sealed with a metal or soft gasket. The union exists for service: loosen it and the whole stem-and-packing assembly lifts out for repacking, trim inspection or seat work, with the body — and the line — undisturbed.
Union designs also dominate the higher classes: 6,000 psi (414 bar) as the standard series and 10,000 psi (690 bar) in the high-pressure families, in stainless and exotic alloys.
The construction resists accidental disassembly under pressure and puts the packing below the power threads, protecting lubricant from the media.
The cost is price, envelope and one more sealing joint — a fair exchange where the valve will be opened, adjusted or repacked during its service life.
What packing sets the temperature ceiling?
Whatever the bonnet, the packing sets the thermal ceiling and much of the stem life. PTFE is the standard: chemically inert, low friction, good to about 450 °F (232 °C).
Above that, graphite (Grafoil) takes over — to roughly 700 °F (371 °C), with high-temperature constructions rated far higher still — at the cost of higher operating torque. Between them sits PEEK for demanding middle ground. A PTFE-packed valve in steam service is a slow leak waiting for a calendar — specify graphite and say so.
Pair the packing with a non-rotating lower stem, which eliminates the grinding that shortens both packing and seat life. Specify blowout-proof back-seated stems anywhere the operator or process is at risk.
What goes wrong, and what do I change?
Most HP needle valve trouble is a packing or trim decision, not a body failure. The symptom points at the cause.
| Symptom | Most likely cause | What to change |
|---|---|---|
| Stem weeping on hot service | PTFE packing run above its ~450 °F (232 °C) ceiling | Change to graphite packing, ~700 °F (371 °C) and beyond |
| Packing and seat wear despite retightening | Rotating lower stem grinding the packing on every turn | Specify a non-rotating lower stem |
| Control drifts, the setting will not repeat | Needle tip deformed by forcing the handle past finger-tight | Replace the trim; stop at finger-tight |
| Weep at the body joint | Union joint gasket or threads disturbed at the last repack | Reseat the union; plan the next repack around the valve |
| Trim work needed with the line live | Integral bonnet on a point that does get serviced | Take the valve off the line, or change construction at rebuild |
What do I put on the RFQ?
Steps 1 to 5 run in this order; each one narrows the construction before you commit to a family.
- Fix the duty pattern. Will the valve be set once, or opened, adjusted and repacked? That answer alone picks the bonnet family.
- State the pressure class. 6,000 psi (414 bar) as standard, 10,000 psi (690 bar) where the line demands it; above 6,000 psi the union family is the route.
- Set the temperature, then the packing. PTFE to about 450 °F (232 °C), graphite to roughly 700 °F (371 °C) and beyond, with PEEK between.
- Specify the stem features. Non-rotating lower stem, and blowout-proof back-seated stem where the operator or process is at risk.
- Fix ends and send the data. SS304 or SS316, NPT, compression or weld ends, with pressure class, temperature, media and end connections stated.
Check the list before the enquiry goes out:
- Bonnet construction chosen, with the reason recorded — service access or class
- Pressure class stated in psi and in bar
- Temperature stated, and packing matched to it
- Stem features stated: non-rotating lower stem, back-seated blowout-proof stem
- Body material, end connections and media stated
FerruleX supplies high-pressure stainless needle and globe-pattern valves in SS304 / SS316 with NPT, compression and weld ends. Start from the needle valve category or the high-pressure female valve and weld-end needle valve styles, and send pressure class, temperature, media and end connections. Request a factory quote.
For the metering mechanism these valves carry, see how does a needle valve work; for the material side of the same spec — 316 vs 17-4 PH stems, PTFE vs graphite packing — see valve trim materials explained.
FAQ
What is the difference between integral and union bonnet needle valves? Integral bonnets are machined into the body as one piece — compact, fewer joints, economical, but trim service means removing the valve. Union bonnets join by a threaded union, so the stem assembly lifts out for repacking in place.
What pressure class are high-pressure needle valves? Integral designs commonly run to about 6,000 psi (414 bar). Union families cover 6,000 psi as standard and extend to 10,000 psi (690 bar). State the class and temperature on the RFQ.
Which packing should I specify? PTFE to about 450 °F (232 °C) for most instrument duty. Graphite for roughly 700 °F (371 °C) and beyond, with PEEK between the two. The wrong packing fails quietly as stem leakage.
Can I repack a needle valve in the line? Union bonnet valves, yes — that is what the union is for. Integral bonnets allow packing adjustment through the stem hardware, but deeper trim work means removing the valve.
Are these the valves for shutoff duty too? At instrument scale they close positively, but metering valves live longest metering. Pair the needle valve with a ball valve for isolation, and never force the handle past finger-tight.