Steam service is the first duty that makes a generic valve datasheet tell the truth about itself. The short answer: a 316 body carries steam duty comfortably, and the real limits sit in the seat, the packing and the gasket. Name the steam state on the RFQ — saturated or superheated — and the specification follows from it.
Key takeaways
- Saturated steam locks temperature to pressure: about 120 °C at 1 barg, about 184 °C at 10 barg, about 215 °C at 20 barg.
- Superheated steam is heated past its saturation temperature for the pressure — drier, and harder on every elastomer, polymer and lubricant in the valve.
- 316 bodies carry steam duty comfortably; the limits live in PTFE seats and PTFE packing, with carbon-filled PTFE or PEEK and graphite packing above their classes.
- Wet steam erodes: droplets abrade like sand, and condensate slugs make water hammer.
- Slow warm-up, sloped lines and steam traps at low points prevent the hammer; the valve spec starts with steam state, pressure and superheat degrees.
Which steam are you actually buying for?
Saturated steam is the easy case to describe and the dangerous one to assume. Pressure and temperature are the same fact read two ways: raise the pressure and the temperature is locked to it. The pairs worth carrying are about 120 °C at 1 barg, about 184 °C at 10 barg, about 215 °C at 20 barg — standard steam-table values.
That is why a valve “rated to 200 °C” is a specific claim about saturated service. It covers the 1-to-roughly-12-barg band and stops there, whatever the body class says. Saturated steam in practice also arrives wet — a few percent moisture by mass is normal — and those droplets are the erosion and hammer story below.
Superheated steam starts as saturated steam and is heated further, past the saturation temperature for its pressure. The degrees above saturation are the superheat. Pressure and temperature are now independent dials, so a superheated line can be modest in pressure and brutal in temperature — which is what makes it the harder duty of the two.
| Duty | Temperature against pressure | Effect on the valve | Decisive column |
|---|---|---|---|
| Saturated | locked to pressure: about 120 °C at 1 barg, 184 °C at 10 barg, 215 °C at 20 barg | limit is predictable from the pressure line alone | the pressure line decides the whole spec |
| Saturated, wet | same, with a few percent moisture by mass | droplets at velocity erode seats and elbows like sand | dryness, not temperature |
| Superheated | independent, in degrees above saturation | dry heat bakes packing and ages every polymer | the degrees of superheat decide, not the pressure |
What decides it: seat and packing, not the body
For saturated steam at ordinary pressures the honest build is a 316 or CF8M body — corrosion resistance and weld behaviour are settled territory, per the stainless steel grades chart — with a seat and packing chosen to the same temperature.
PTFE is the decision point. Its practical continuous ceiling sits near 200–230 °C depending on grade, which places 10 barg saturated steam — about 184 °C — inside but close to the boundary. Anything superheated is potentially past it.
Maker practice splits here. Some rate carbon-filled PTFE seats for defined saturated-steam working pressures; others direct steam duty to PEEK above the PTFE class. The honest move is to quote the maker’s steam rating for the exact seat rather than assume it.
Above the polymer classes sit graphite packing, graphite gaskets and metal-seated valves for the genuinely hot work. Seat logic is the same conversation as ball valve seat materials, and the packing side is valve packing and fugitive emissions.
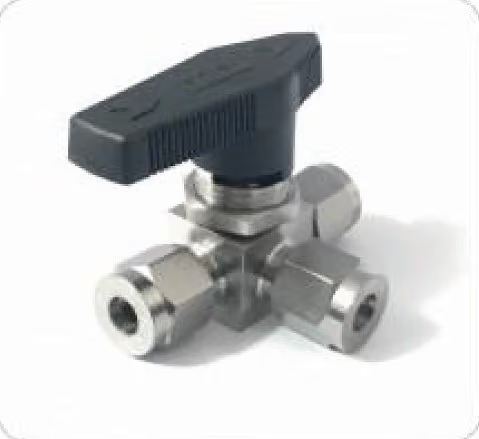
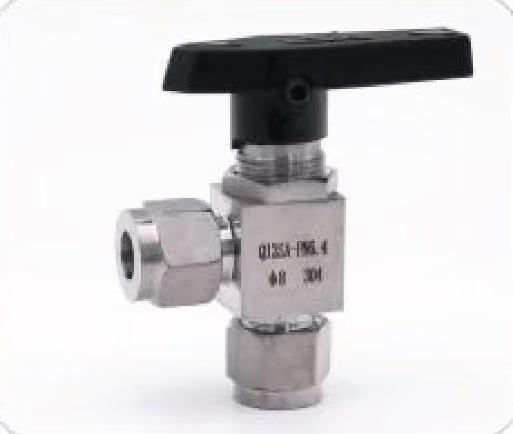
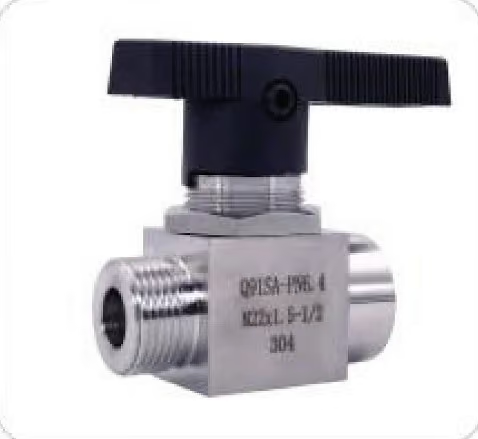
Steam service is where both posts meet. Our ball valves carry defined steam working pressures where the seat allows.
What fails first?
Superheat punishes the soft parts first. The industry consensus, echoed across seal and valve references, is that elastomers and polymer seats fail before any metal does. Dry heat ages them fast, heat travels up the stem and bakes the packing, and lubricant films collapse where steam provides none.
The further the superheat, the more the valve’s real specification migrates from the body to the seat, the packing and the gasket.
| Symptom | Most likely cause | What to change |
|---|---|---|
| Gland leaks after a hot run | PTFE packing baked dry up the stem | graphite packing |
| Seat creeps, shut-off drifts on a superheated line | polymer seat above its temperature class | PEEK seat, or a metal-seated valve |
| Seat and elbow wear with no hammer | wet steam droplets at velocity, eroding like sand | line dryness and trap placement |
| Pressure spike at the valve on warm-up | condensate slug arriving at the valve | line slope, traps at low points, slower warm-up |
| Gasket weeps under thermal cycling | gasket class below the duty | graphite gasket |
How do I keep condensate from wrecking the valve?
Steam’s liquid shadow decides more failures than the steam does. As steam gives up heat it condenses; condensate pools in low points, slugs of water accelerate in the line, and a slug arriving at a valve or elbow converts its momentum into a pressure spike — water hammer. A hammered plant is almost always a trapped-warm-up failure, not a valve failure.
- Slope the lines so condensate runs to the low points.
- Put steam traps at those low points.
- Crack the valve and let the traps clear the cold condensate.
- Bring pressure up gradually rather than opening into a cold line.
- Keep the line dry where hammer is absent — droplets at velocity still erode seats and elbows the way the references put it, like sand.
What do I put on the RFQ?
steam state— saturated, or superheated with degrees of superheat.pressure and temperature— both, even though saturated ties them; the pair states the line class.dryness— if known, especially for turbine or meter-feed duty.cycle count— thermal cycling drives seat and packing selection as much as the steady state.seat and packing— ask for the maker’s steam rating for the exact seat, not the generic temperature line.gasket— graphite where the polymer classes are exceeded.
FAQ
Can I use a PTFE seat valve on 10 barg steam?
Ten barg saturated is about 184 °C, inside virgin PTFE’s practical class but close enough to the ceiling that the maker’s steam rating for that exact seat must decide, not the generic temperature line.
What is the difference between saturated and superheated steam?
Saturated steam’s temperature is locked to its pressure: 184 °C at 10 barg, always. Superheated steam is heated past that curve, so the two are independent and it runs dry and hot. Pressure alone predicts saturated limits, not superheated ones.
Why does superheat damage seals first?
The soft parts have the lowest ceilings and dry heat ages them fastest. Elastomers embrittle, polymer seats creep, packing bakes dry up the stem, and steam supplies no lubrication. Body metal tolerates what the seals cannot.
How do I prevent water hammer in a steam line?
Slope the pipe so condensate reaches low points, trap every low point so it never pools, and warm the line slowly — crack the valve, clear the cold condensate, raise pressure gradually. Hammer is condensate physics, not valve quality.
Does steam corrode 316 stainless?
Not the way chlorides do. 316’s steam-side enemy is heat plus stress — the territory of chloride stress corrosion cracking where chlorides concentrate — and erosion where wet steam runs fast. Clean, dry steam is gentle to 316.