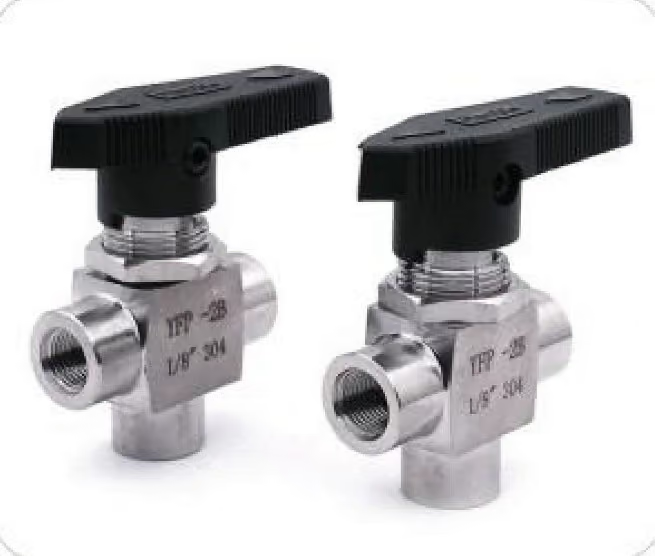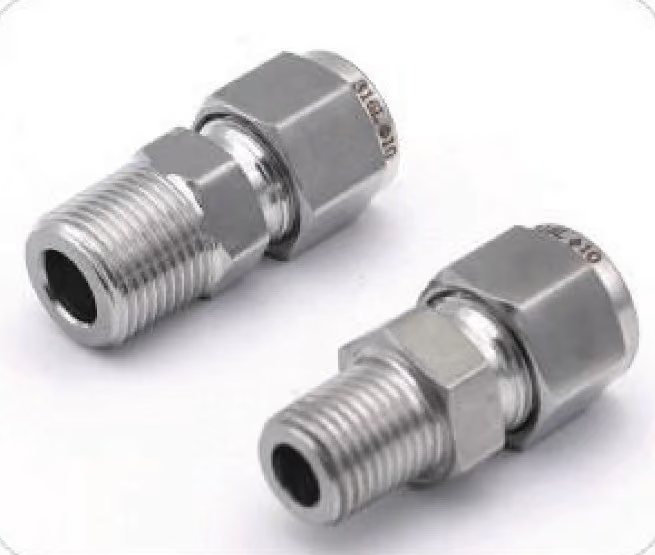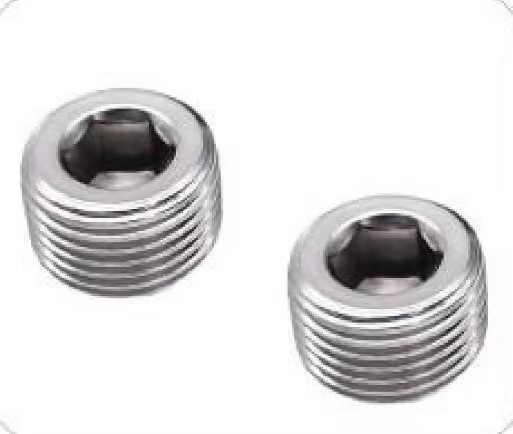
Thread galling is the cold-welding seizure that happens when two stainless steel threads are tightened against each other: the protective oxide film breaks at the contact points, friction heat welds the bare metal together, and the joint locks solid — often twisting off or tearing threads before it lets go.
Austenitic stainless is among the most galling-prone of metals, so the fittings that resist corrosion best are the ones most likely to seize at assembly. Three things prevent it: lubricant the service allows, slow final turns, and never forcing a doubtful thread. A galled joint is a scrap joint, and no amount of rework makes it sound again.
Key takeaways
- Galling is adhesive wear: oxide film on the threads breaks under load, bare metal spots weld from friction heat, and the weld rips material out of the softer side — stainless-on-stainless is the classic pairing because both surfaces carry the same film and similar hardness.
- Stainless NPT into a stainless port is a high-risk joint: the taper wedges the flanks together as it tightens, multiplying contact pressure and sliding friction.
- Prevention beats repair: a process-compatible lubricant or anti-seize, slow tightening, clean undamaged threads, correct torque, and — where the design allows — a dissimilar or harder mating pair.
- A galled joint is a scrap joint: the metal is torn and transferred, loosening re-damages it, and the reliable fix is replacement of the fitting, with the port inspected and repaired only by an approved method.
Which joints do I need to treat as high risk?
Most metals gall under the wrong conditions, but austenitic stainless — 304, 316, 316L — is the repeat offender. Its corrosion resistance comes from the same oxide film that makes it prone to adhesion. Thread contact pressure and friction shear that film off the high points, and bare stainless then meets bare stainless.
The identical crystal structures bond readily. Stainless also dissipates friction heat poorly and runs a high coefficient of friction, so the heat that drives the micro-welds builds fast. The damage is cumulative: each pass tears material, roughens the flanks, enlarges contact area, and builds stronger bonds until the joint seizes.
On a fitting line it shows at the obvious places: compression nuts running onto stainless bodies, NPT adapters threading into stainless valve ports, plugs and bleed fittings seated after a long service interval. The taper makes NPT the worst case. Every additional turn wedges the flanks harder, so the joint generates more friction precisely as engagement increases.
Which thread form you are dealing with matters too, since the taper does part of the sealing work — the identification guide is NPT vs G (BSP) threads.
Which prevention lever do I actually need?
| Lever | What it prevents | Trade-off | What decides it |
|---|---|---|---|
| Process-compatible lubricant or anti-seize | Friction and metal-to-metal contact; the single most effective measure | Must suit the service — oxygen, food and high-purity lines restrict chemistry; lubrication changes torque-to-load, so use torque values for the lubricated condition | The service chemistry. If the line cannot take a lubricant, this lever is closed to you |
| Slower tightening | Friction heat; power-driving stainless is the classic trigger | Adds seconds per joint; use hand tools or low-speed drivers on final engagement | How the joint is driven — hand tools or a low-speed driver on the final turns |
| Clean, undamaged threads | Debris and roughness that seed galling | Inspection time; reject burred or previously galled parts rather than forcing them | Incoming inspection, not process — you cannot torque your way out of a burr |
| Correct torque, no over-tightening | Contact stress that drives adhesion | Under-tightening leaks — follow the fitting maker’s torque or turn-of-nut guidance | The maker’s torque or turn-of-nut guidance, read for the lubricated condition |
| Dissimilar or harder mating pair | Like-on-like adhesion — a harder or different-alloy partner work-hardens differently and bonds less | Needs design freedom: 304 against 316, or a plated/hardened component; confirm corrosion and strength still fit the service | Design freedom at specification stage — available before the joint is drawn, not after |
In practice the first three levers cover most field problems: lubricate what the process allows, run the last turns slowly by hand, and never force questionable threads. Where the duty is repetitive — production panel assembly — pre-applied dry-film lubricant or batch-applied anti-seize removes the on-site variable.
Torque discipline is part of good installation practice, walked through in how to install compression fittings.
What do I check on the parts before assembly?
- Thread form and size confirmed against the port, not judged by eye.
- Flanks clean and free of debris, cutting oil or old sealant.
- No burrs and no roughness on the high points of the thread.
- No part that has already galled — reject it rather than dressing and reusing it.
- Port threads inspected on the same terms as the fitting.
- Service chemistry confirmed before a lubricant is chosen.
How do I assemble the joint without galling it?
- Inspect both thread sets. Reject burred, rough or previously galled parts before they reach the line; roughness seeds adhesion.
- Confirm the thread form and the port condition. A mismatched or damaged port will make any lubricant strategy fail.
- Apply the lubricant, if the service allows it. A process-compatible anti-seize or lubricant on the threads keeps the oxide films apart.
- Engage by hand first. The first turns tell you whether the threads are running true; a joint that fights from the start will not seat cleanly.
- Run the final turns slowly. Hand tools or a low-speed driver only — a fast power driver is the classic trigger for friction heat.
- Torque to the maker’s value and stop. Do not add turns to chase a leak; over-tightening raises contact stress and drives adhesion.
What went wrong if the joint seized?
| Symptom | Most likely cause | What to change |
|---|---|---|
| Torque climbs and the joint stops part-way on assembly | Oxide film broken at the contact points, bare metal welded by friction heat | Stop. Scrap the fitting, then lubricate and slow the next assembly |
| NPT adapter welds into a stainless port | The taper wedges the flanks harder with every extra turn | Service-compatible sealant or anti-seize; stop at proper engagement, do not force extra turns |
| Threads grab on the last turns when power-driven | Friction heat from high-speed driving | Hand tools or a low-speed driver on final engagement |
| Torn, smeared metal; rising torque instead of release | Galling — adhesive seizure | Replacement. Inspect the port; repair only by an approved method |
| Sheared crests and the joint spins free | Stripping — mechanical overload, a different failure from galling | Replacement; then check the torque and thread condition that caused the overload |
| Galling recurring at the same joint | The process is unchanged: no lubricant, fast assembly, like-on-like pair | Change the lubrication, slow the assembly, or change the mating pair |
| Galled threads dressed and put back into service | Torn and transferred metal that re-damages the sealing faces on retightening | Do not reuse. Fit a new part |
A joint that seizes mid-assembly, or one that resists removal with rising torque, is telling you the surfaces have welded. Do not power through: forcing it twists off fittings, wrecks ports, and sends debris into the line. The prognosis is replacement. Galled metal is torn and transferred, and loosening then retightening just re-damages the sealing faces.
Inspect both sides: the fitting is usually scrap, and a galled port is repaired only by an approved method. Note the difference from stripping — galling seizes from adhesion with torn, smeared metal; stripping spins free from overloaded threads with sheared crests. One locks, one slides.
FerruleX quotes compression fittings, plugs and adapters with threads machined and cleaned for assembly — and we will pre-apply anti-seize or specify a dissimilar pairing on request where the service allows it. Name the thread standard, the service and any lubrication restriction on the RFQ. Request a factory quote.
Can I select a grade to remove the risk?
Treat grade selection as one lever among several, not a cure. The austenitic grades that make up most fittings can all gall, and published galling-threshold test tables show the outcome is pairing-specific — the tables give no dependable ranking of 304 against 316.
What the data does support: Nitronic 60 (UNS S21800) exists specifically as a galling-resistant stainless. One maker’s threshold table shows it holding past 50 ksi (345 MPa) against Type 304, where stainless-on-stainless pairings score far lower. That is why it is the standard upgrade for stuck-prone studs and valve trim.
Free-machining 303 trades corrosion resistance for machinability, so it is not a shortcut for corrosive duty. 17-4 PH’s behaviour varies with heat-treat condition and mating grade. The honest summary: pair by test data, not by folklore — and when the pairing is fixed, the lubrication and assembly levers above do the rest.
FAQ
How do you fix galled threads? Replace the fitting. Galling tears and transfers metal, so loosening and reusing re-damages the sealing faces. Have the port inspected and repaired only by an approved method such as re-tapping within limits.
What is the difference between thread galling and stripping? Galling is adhesive seizure: friction welds the surfaces and the joint locks or drags, with metal torn and smeared. Stripping is mechanical overload: the threads shear and the joint spins free.
What lubricant prevents stainless thread galling? Any process-compatible anti-seize or lubricant that keeps the oxide films apart — molybdenum-disulfide, graphite, PTFE-based or proprietary anti-galling compounds are the usual choices. Service chemistry is the constraint, and lubricated joints need torque values calculated for the lubricated condition.
Are NPT threads into stainless ports especially prone to galling? Yes. The taper wedges the flanks harder as engagement increases, raising contact pressure and sliding friction together. Slow assembly, a service-compatible sealant or anti-seize, and stopping at proper engagement are the standard defences.
Can I mate stainless threads to stainless threads at all? Yes, with discipline — most stainless threaded joints assemble fine when lubricated, run slowly, clean and torqued correctly. A dissimilar pairing removes much of the risk where the duty allows it.
Which stainless grades gall the most — does switching grades help? Grade selection is one lever, not a cure: the austenitic grades can all gall, and the outcome is pairing-specific. Nitronic 60 (UNS S21800) is the galling-resistant option where the pairing is fixed.