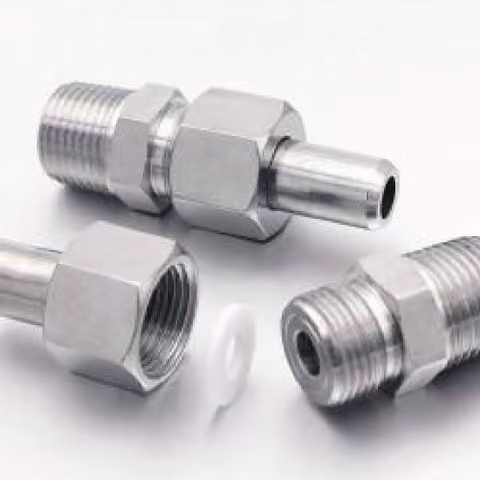
Weld Straight Connector
Weld Straight Connector: stainless weld-end pipe/tube connector for permanent joints. SS304/316. FerruleX RFQ. Stocked sizes ship fast. Fast stock shipping.
- Brand
- FerruleX
- Material
- SS304 / SS316
- Type
- Weld straight connector
- Ends
- Weld (options per RFQ)
- Order mode
- Factory RFQ / OEM
- Stock5–7 days after confirmation
- Make to order15–25 days production
- Payment / termsT/T ~30% or L/C · FOB Shanghai / Ningbo
- OEMLogo and drawings accepted · price on RFQ
Description
Both ends of this straight body are prepared for welding; a threaded variant adds a threaded end where a valve has to come apart for service. Body stock is 304 or 316, spanning 1/8 in to 2 in, M5 to M36 and 10 mm to 27 mm tube OD, with ZG(R), NPT, G and M threads on the threaded end. Working pressure runs around 3000 psi in liquid or gas service, though the weld procedure and the pipe wall at the joint decide the real limit, so the schedule goes on the RFQ beside the size. The bore is straight through in every case.
End prep is the buyer side of the job: bevel, root gap and purge are set by the weld procedure, not by the part. The part supplies the straight bore, weld land and material, 304 or 316, 1/8 in to 2 in. A threaded end is cut in ZG(R), NPT, G or M and masked against spatter.
- End forms
- Welded at both ends for a permanent joint, or welded on one side and threaded on the other.
- Alloy
- 304 or 316 stainless for the body.
- Sizes
- 1/8 in to 2 in, M5 to M36, and 10 mm to 27 mm tube outside diameter.
- Threads
- ZG(R), NPT, G or M where a threaded end is called off.
Specifications
| Specification | Value |
|---|---|
| Brand | FerruleX |
| Material | SS304 / SS316 |
| Type | Weld straight connector |
| Ends | Weld (options per RFQ) |
| Order mode | Factory RFQ / OEM |
Request Quote
Prices stay on the RFQ. Send size, material, quantity and destination — the factory replies with price, lead time and packing. Packing, payment and the usual quote questions are on thedelivery pageand the FAQ.
Questions about this part
What does the fitting supply at the weld end and what do we set?
The body supplies the bore, the weld land and the alloy, 304 or 316. Bevel angle, root gap and purge are set by your weld procedure, not by the part. Send the procedure with the RFQ so the end prep matches it.
Is the weld end a socket joint or a butt prep?
That is fixed at order, so state it plainly. A socket end takes the tube over a shoulder and is fillet welded; a butt end meets the tube face and needs a square cut and a gap. The two are not interchangeable.
With one welded end and one threaded end, which goes first?
Weld first, then make up the thread. Heat and spatter ruin a machined thread, so the threaded end is masked or left until the welded side has cooled and been cleaned. Say which end is welded on the drawing.
Does the joint need pickling or passivation after welding?
The weld and its heat tint have to be cleaned, otherwise the chromium depleted zone stays open to corrosion. Pickling paste or a pickling bath removes the tint; passivation follows to restore the passive film. Both belong to the weld procedure, not the fitting.
Are NPT, BSPT and BSPP interchangeable on the threaded end?
No. NPT is the American taper, BSPT is the taper behind ZG(R), and BSPP is the parallel G thread; the thread forms and pitch differ, so a male NPT will not seal in a female BSPP port. Call the form you need.
How should the threaded end be sealed and kept from galling?
Stainless threads gall when run dry, so use a nickel or PTFE based anti-seize or PTFE tape on the male thread and keep spatter off it during welding. Hand tight plus a part turn is enough on a taper; do not over-torque.
Related products
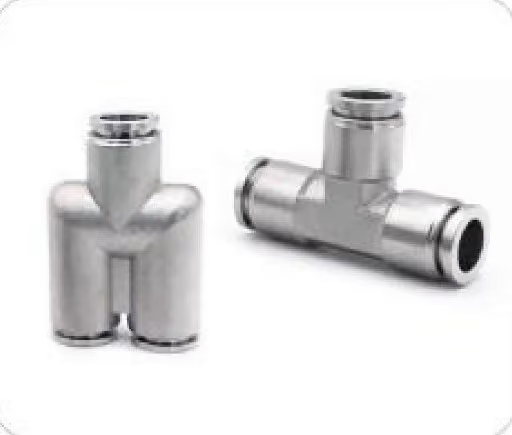
Y-Type and T-Type Tee Fitting
Y-Type and T-Type Tee Fitting: stainless Y/T branching pipe fittings, NPT/G/metric. FerruleX RFQ. Stocked sizes ship fast. Export RFQ only — no cart.
View details →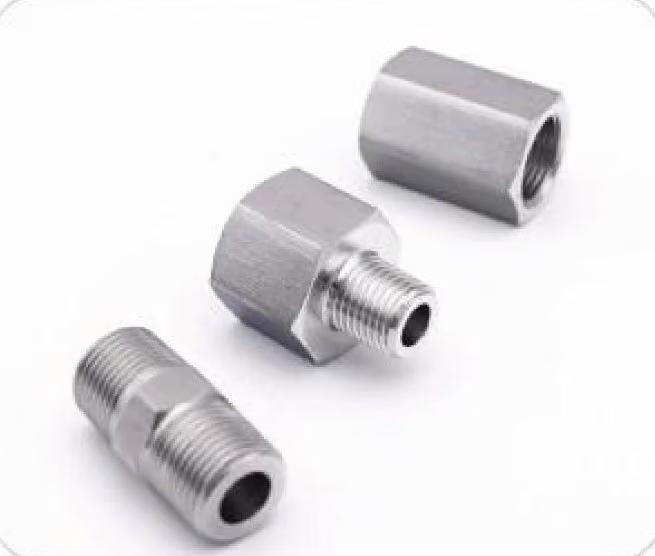
Male-Female Straight Adapter
Male-Female Straight Adapter: stainless steel pipe fittings converting NPT/G/metric threads. FerruleX RFQ. Stocked sizes ship fast. Export RFQ only — no cart.
View details →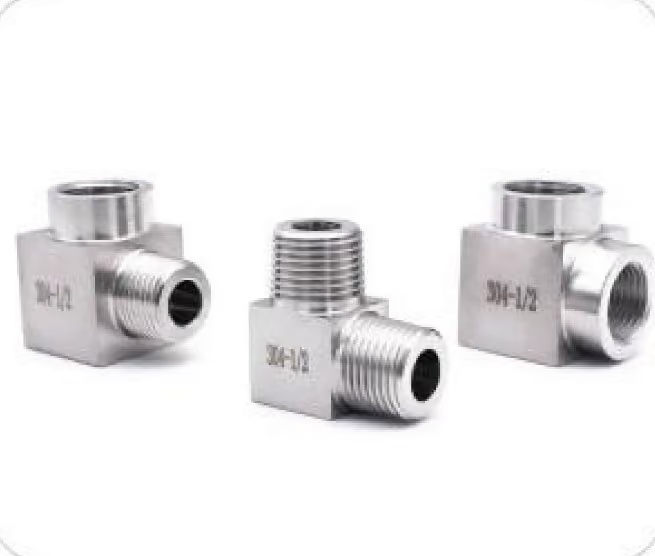
Stainless Steel Male-Female Elbow Adapter — Sizes
Male-Female Elbow Adapter: 90° stainless steel pipe fittings changing thread gender/standard. FerruleX RFQ. Stocked sizes ship fast. Export RFQ only — no cart.
View details →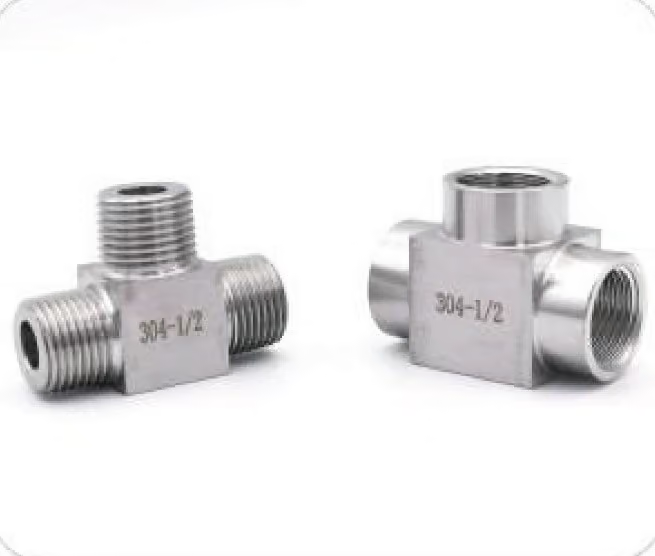
Female Threaded Tee
Female Threaded Tee: all-female stainless steel pipe fittings for branching headers. FerruleX factory RFQ. Stocked sizes ship fast. Export RFQ only — no cart.
View details →