Tri-clamp gaskets are the least-discussed third of every sanitary joint — the clamp supplies the squeeze, the ferrules supply the faces, and the gasket does the actual sealing.
A gasket is bought by three names: the nominal size of the joint, the ferrule standard, and the compound. The size names the fitting, not the gasket — a 2 in gasket measures about 1.900 in ID and 2.520 in OD. The compound is decided by the cleaning cycle before the product.
Key takeaways
- A tri-clamp gasket is named for the fitting’s nominal size, not its measured diameter — a “2 inch” gasket measures about 1.900 in ID and 2.520 in OD.
- Flange sharing is real: 1/2 and 3/4 in joints use one 0.860 in OD mini-gasket (different IDs), and the 1 in and 1-1/2 in flanges both sit near 1.98 in OD — which is why the named size must travel with the order, not the measured one.
- ASME BPE, DIN 32676 and ISO 2852 ferrule systems are not dimension-for-dimension interchangeable; a “2 inch gasket” without the standard named is an incomplete callout.
- Materials divide on sterilization: EPDM is the usual steam-in-place (SIP) and caustic CIP choice; silicone is conditional for steam; PTFE covers the widest chemistry but cold-flows; standard FKM grades are not for continuous SIP or hot caustic.
- Certifications follow the compound, not the polymer: FDA 21 CFR 177.2600 (rubber), 177.1550 (PTFE), USP Class VI and 3-A are claims about a specific product from a specific maker.
Which gasket do I need?
Three answers settle it: the nominal size of the joint, the ferrule standard it must seat in, and the compound your cleaning cycle allows. Get one wrong and the joint leaks, blows out, or hardens into the contamination source the sanitary design was built to avoid.
| Decision | What actually settles it | The usual mistake |
|---|---|---|
| Which size | Nominal size of the ferrule and pipe joint, read off the fitting system’s table | Measuring the old gasket and rounding |
| Which standard | The flange it has to seat in: ASME BPE, DIN 32676 with its series, or ISO 2852 | Quoting “2 inch” with no standard named |
| Which compound | The cleaning cycle first — CIP chemistry and SIP steam — the product second | Choosing on the polymer’s reputation |
The joint itself is two ferrules — tube stubs ending in raised flanges — with the gasket seated between the faces, centred in the bore, and a clamp pulling the flanges together around it. The clamp is the load source, the gasket the seal element, and the ferrule faces define where compression lands.
No threads, no welds at the joint, which is why the system dominates food, beverage, dairy and bioprocess lines. The joint anatomy and the ferrule measuring procedure are covered in what are tri-clamp fittings.
The gasket is the consumable in that system — replaced at teardown intervals, and the part whose condition quietly decides whether the joint holds pressure and stays crevice-free. Its material governs cleanability as well: a gasket that survives CIP chemistry but hardens in steam becomes the contamination source the design was meant to avoid.
How is a tri-clamp gasket sized?
The sizing convention is the single biggest ordering trap. A tri-clamp gasket is specified by the nominal pipe/ferrule size of the joint — and that nominal number matches no dimension on the gasket:
| Nominal size | Approx. ID (in) | Approx. OD (in) | Approx. thickness (in) |
|---|---|---|---|
| 1/2 | 0.370 | 0.860 | 0.085 |
| 3/4 | 0.620 | 0.860 | 0.085 |
| 1 | 0.900 | 1.984 | 0.085 |
| 1-1/2 | 1.400 | 1.980 | 0.185 |
| 2 | 1.900 | 2.520 | 0.185 |
| 2-1/2 | 2.400 | 3.050 | 0.185 |
| 3 | 2.900 | 3.580 | 0.185 |
| 4 | 3.870 | 4.680 | 0.185 |
Approximate catalog dimensions — they vary by profile and maker tolerance, so confirm per order rather than machining to them. Read the pattern, not the digits: the ID runs close to (slightly under) the nominal bore, and the “2 inch gasket” nobody can find is the one measuring 1.900 in.
The shared-flange quirks are worth memorising. The 1/2 and 3/4 in joints take the same 0.860 in OD gasket — the “mini” gasket — differing only in ID. That is why a mixed 1/2-to-3/4 assembly uses the larger-ID gasket with the same flange.
The 1 in and 1-1/2 in flanges both land near 1.98 in OD, which is why those two sizes interchange clamps. In both cases the rule is the same: order by named size, and when joining different tube sizes that share a flange, use the larger gasket so the bore has no unsealed gap.
To identify the size you need:
- Measure the ferrule flange OD and the tube OD.
- Identify the nominal size from the fitting system’s table.
- Check whether the flange is shared — 1/2 with 3/4, or 1 with 1-1/2.
- Confirm the standard and series the flange belongs to.
- Order by the nominal name, not the measured diameter. Measuring a used gasket and rounding is how wrong gaskets get ordered.
Which standard does my flange follow?
Sanitary ferrule systems are regional, and their gaskets do not cross over freely:
- ASME BPE — the North American bioprocessing standard; dimensions in inches, as in the table above.
- DIN 32676 — the European standard, dimensioned on metric tube ODs, and itself split into series A, B and C — a “DIN clamp gasket” without a series is as incomplete as an NPT callout without a size.
- ISO 2852 — the international attempt, close to but not interchangeable with either at every size.
A 2 in ASME BPE gasket will not reliably seal a DIN flange: flange OD, groove geometry and gasket thickness differ across the systems.
The RFQ-proof callout names all of it — standard, series where applicable, nominal size, material, profile. For example: gasket, ASME BPE, 2 in, EPDM or DIN 32676 series B, DN25–OD34, silicone.
Which material for my cleaning cycle?
Published temperature ranges for sanitary gasket compounds — treat them as typical ranges for the compound family and verify the specific product rating for your duty:
| Material | Typical range | Decisive condition | Stands out in | Watch out for |
|---|---|---|---|---|
| Silicone (VMQ) | −100 to 400 °F (−73 to 204 °C) | No repeated steam — steam rating is per compound | Low extractables, wide temp, high-purity water duty | Steam is conditional — repeated SIP hardens many grades; poor resistance to acids, alkalis, solvents, oils, abrasion |
| EPDM | −50 to 300 °F (−46 to 149 °C) | Repeated SIP steam and water-based caustic CIP | Steam and hot water — the usual SIP elastomer; water-based caustic CIP; dilute acids and alkalis | Fails in mineral oils, hydrocarbons, greases — one lubricated fitting ruins it |
| PTFE (solid) | −100 to 500 °F (−73 to 260 °C) | Aggressive chemistry, and the joint holds compression | Broadest chemical resistance — acids, alkalis, solvents, oxidizers; lowest extractables | No elasticity: cold-flows under sustained clamp load, sensitive to under-compression and misalignment |
| FKM (fluoroelastomer) | −20 to 400 °F (−29 to 204 °C) | Oil, fuel or solvent contact at moderate temperature | Oils, fuels, many solvents and acids | Standard grades are not for continuous SIP or hot caustic CIP — special grades exist, verified per compound |
| Buna-N (NBR) | −30 to 200 °F (−34 to 93 °C) | Oil and grease only, with no SIP duty | Oils and greases at modest temperature | Not for repeated SIP or hot caustic; ozone and heat aging limit service life |
Three of those rows carry the decisions most plants get wrong. Silicone’s steam tolerance is conditional — the common assumption that silicone handles SIP by default is a simplification. EPDM and PTFE take repeated steam notably better, and a silicone grade rated for steam is a per-compound question.
EPDM’s weakness is oils — excellent in everything water-based, degraded by hydrocarbon contact. PTFE’s weakness is mechanical, not chemical — it creeps, so a solid PTFE gasket in a joint that cycles temperature or gets under-clamped will relax its seal even while chemically intact.
What does an envelope gasket change?
The envelope gasket answers the “PTFE chemistry but elastic sealing” problem with a two-part construction: a PTFE shell facing the product wetted surfaces, wrapped around an elastomer core — typically EPDM or FKM — that provides the compression and recovery. The shell takes the chemistry; the core takes the mechanics.
- The temperature limit belongs to the core, not the shell — the assembly is limited to roughly the elastomer’s range, not PTFE’s 500 °F. Specifying an envelope gasket by the shell rating overstates the joint.
- The assembly is only as certified as its whole — shell integrity is a wear item (a cracked or perforated jacket ends the gasket’s life), core compatibility must be checked against the media independently, and certifications apply to the finished item, not to “PTFE + EPDM” as a concept.
Envelopes earn their place where aggressive cleaning chemistry or product contact rules out plain elastomers — WFI systems, bioprocess skids, solvent duty.
What about screen and orifice gaskets?
Two functional variants show up in sanitary lines, both gasket-plus-device hybrids:
- Screen (mesh) gaskets — a stainless mesh disc sealed into the gasket profile, adding coarse inline straining to the joint: catching scale, weld beads and debris ahead of pumps, valves and instruments. Useful as a guard, but not a validated filter — expect a pressure drop, monitor it, and treat clogging as the maintenance signal it is.
- Orifice (restrictor) gaskets — a gasket with a reduced center bore, providing a fixed restriction for flow balancing, pressure drop, or branch equalization. The restriction is fixed — flow still moves with conditions — so it complements rather than replaces adjustable flow control.
What goes wrong, and what do I change?
Most change-outs trace back to one of these:
| Symptom | Most likely cause | What to change |
|---|---|---|
| Joint weeps after a steam cycle | Silicone grade not rated for repeated SIP — hardened | Move to EPDM, PTFE or an envelope; put SIP pressure, temperature and frequency on the spec |
| Seal relaxes with no sign of chemical attack | Solid PTFE cold-flow under sustained clamp load, worse with under-compression or misalignment | Re-check alignment and compression; an envelope gasket restores recovery |
| Gasket swells or softens | EPDM or Buna-N in contact with mineral oil, hydrocarbon or grease | Move to FKM or PTFE; keep lubricant off the joint |
| Blowout, or an unsealed gap at the bore | Standard mismatch, or the wrong gasket on a shared flange | Name standard and series with the nominal size; use the larger gasket on a shared flange |
| Pressure drop climbing ahead of a pump, valve or instrument | Screen gasket clogging on scale, weld beads and debris | Clean or replace the mesh gasket and watch the pressure drop |
| Envelope gasket fails early | Cracked or perforated PTFE jacket, or a core outside the elastomer’s range | Check shell integrity and core compatibility separately |
What goes on the specification?
A complete gasket specification is six lines: standard and series, nominal size, material (compound, not just polymer), certification requirements, process media, and the cleaning regimen — CIP chemistry and temperature, SIP pressure and frequency.
That last pair is where most material mistakes enter: the gasket that survives the product but not the cleaning cycle is still the wrong gasket.
- Standard and series — ASME BPE, DIN 32676 series A/B/C, or ISO 2852.
- Nominal size — the name of the joint, never the measured diameter.
- Material — the compound, with hardness and cure system, not just the polymer name.
- Certification — the compound’s compliance documentation, requested with the batch.
- Process media — the product, and the oils or solvents it carries.
- Cleaning regimen — CIP chemistry and temperature, SIP pressure and frequency.
What do the compliance claims mean?
Gasket compliance claims are compound-specific, and the acronyms get mixed up routinely:
- FDA 21 CFR 177.2600 — rubber articles for repeated food contact: permitted ingredients plus extraction limits in water and fat simulants. It is a materials compliance, not a pressure, temperature or design rating. Note the trap: PTFE is regulated under 21 CFR 177.1550, not 177.2600 — a “FDA silicone” and a “FDA PTFE” gasket are certified under different paragraphs.
- USP Class VI — biological reactivity testing (systemic injection, intracutaneous, implantation) for materials in contact with drugs and devices. It says nothing about food contact, chemical compatibility, or cleanability.
- 3-A — sanitary design criteria for dairy and food equipment, applied at the product level.
The meta-rule: certifications travel with the compound, not the polymer. “EPDM” is not USP Class VI; a specific EPDM compound from a specific maker, tested and documented, is.
When the process demands it, request the compound’s compliance documentation with the batch — hardness, cure system, temperature rating and the certificates as one package.
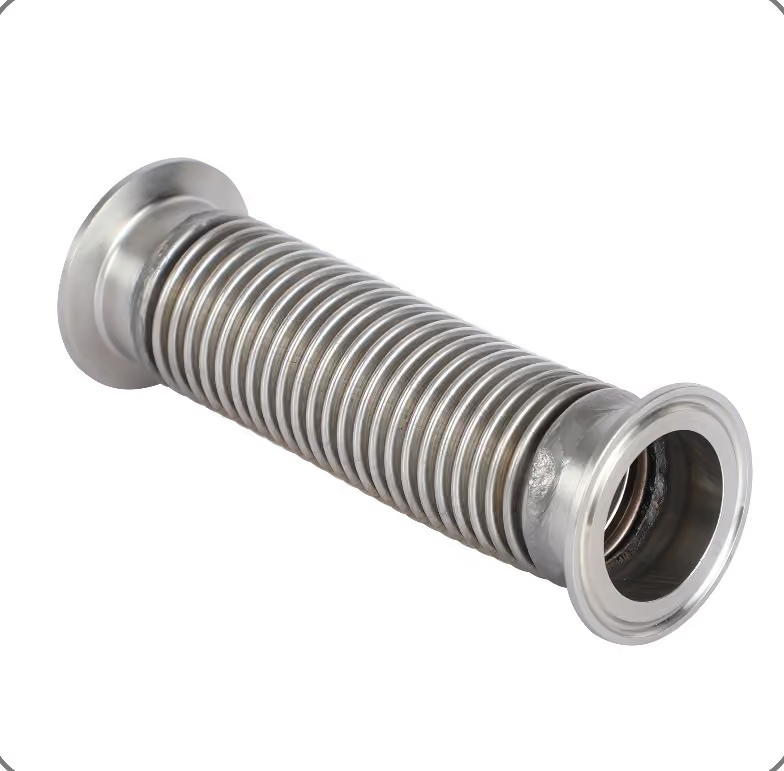
FerruleX works the hardware side of these joints — tri-clamp ends machined into stainless corrugated hose assemblies and the sanitary ranges of the fittings catalog, in 316/316L with surface finishes to match the line.
The gasket specification above is the piece to hand your supplier either way: it is what lets the joint — ours at the hose end, theirs at the gasket — seal to the standard the process was designed around.
Surface-finish context for the rest of the wetted path is in electropolishing vs passivation and our Ra surface finish chart; the valve side of sanitary service is in sanitary ball valves. Send the six-line callout with your enquiry and we will match the ferrule side — contact us.
FAQ
Which gasket material is best for steam sterilization (SIP)?
EPDM, as the general rule: hot water and steam are its strengths, and it is the default SIP elastomer in food and pharma plants. PTFE and envelope gaskets also handle repeated steam. Silicone is conditional: verify the compound’s steam rating.
What is the difference between a solid PTFE and an envelope gasket?
Solid PTFE is chemistry without elasticity: it cold-flows, so flanges must be aligned and properly compressed. An envelope is a PTFE shell over an EPDM or FKM core. Its limit is the core, not the shell’s 500 °F.
Will a 2-inch ASME BPE gasket fit a DIN 32676 ferrule?
Not reliably, and not worth testing: the two systems dimension ferrules and gaskets independently, and flange OD, thickness and profile all differ. DIN itself splits into series A, B and C. Name the standard with the size.
Do all silicone gaskets handle steam sterilization?
No — steam-rated silicone is a compound-level claim. Many grades take occasional SIP, but repeated cycling hardens standard grades. For routine SIP, specify a steam-rated silicone or move to EPDM, and put the SIP cycle on the spec.
Are tri-clamp gaskets sized by their measured diameter?
No — by the nominal size of the joint, which matches no gasket dimension. A 2 in gasket measures about 1.900 in ID and 2.520 in OD. Measure the flange and tube, identify the nominal size, order by that name.