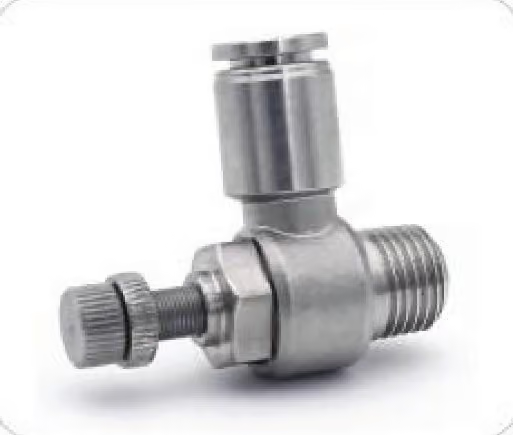
Inline filters are a small body with a porous element that stands between the process and the instrument behind it, catching particles before they reach valve seats, sensing ports and analyzer sensors.
Fit one per instrument leg, at the take-off, where the leg leaves the process. Choose the element by the smallest passage it protects, place it upstream of valves and regulators, and change it on rising differential pressure.
Key takeaways
- New systems are the dirtiest: weld slag, mill scale, rust, chips and sealant residue circulate at start-up and damage valve seats and trim within weeks of operation.
- Element choice is the spec: sintered stainless for fine, cleanable duty; wire mesh at mid ranges; coarse strainers for bulk protection — published ratings run from about 1 µm to 100+ µm in steps that vary by maker.
- Place filters where they protect the instrument: upstream of valves and regulators, at take-off points, ahead of analyzers.
- Rising differential pressure is the element’s service meter — clean elements drop little; a climbing ΔP says the element is loading.
- Sintered elements are cleanable by backflushing, but in small inline bodies replacement is usually the honest economics.
Which element do I need?
The choice is set by the smallest passage you are protecting, not by the filter’s own number. Three element families cover the duty ladder, and the maker’s catalogue decides which numbers exist.
| Element | What it stops | Service it suits | What actually decides |
|---|---|---|---|
| Sintered stainless | Fine particles — published ratings from sub-micron through about 100 µm depending on maker, 5 and 10 µm the common instrument grades | Transmitter ports, valve trim, analyzer inlets | The smallest passage in the protected instrument |
| Woven wire mesh | Mid-range particles, as a cleanable screen | Instrument legs where the element is cleaned rather than renewed | Whether the line needs cleaning instead of replacement |
| Coarse strainer — perforated or heavy mesh | Bulk debris: slag, scale, chips | Take-off and sample lines that start dirty | How much bulk debris the line carries at start-up |
Makers do not share one universal rating ladder. One major catalogue’s sintered set runs 1, 5, 10, 50 and 100 µm, with wire-cloth options at 250 and 450; another’s sintered range steps 0.5 to 90 µm and its strainers run 40 to 440.
So the RFQ line is the job — “protect a transmitter sensing port” versus “strain bulk debris from a sample” — and the maker maps it to the nearest catalogue grade.
Body material is 316 stainless in standard instrument builds, in 1/8 to 1 in threaded forms. Published pressure classes run from 3,000 psig at the common end to 6,000 psig in high-pressure series.
Step 1 — name the smallest passage. Transmitter sensing ports and valve trim gaps are the fine end. A regulator seat guarding bulk debris is the coarse end.
Step 2 — pick the family from that passage. Sintered for fine, woven mesh for mid-range, coarse strainer for bulk.
Step 3 — write the job, not the micron. “Protect a transmitter sensing port” is a cleaner RFQ line than a number, because the ladder is the maker’s.
Step 4 — confirm the body spec. 316 stainless, 1/8 to 1 in threaded, 3,000 or 6,000 psig class.
Step 5 — check the ladder on the maker’s own datasheet. What one catalogue lists as 1, 5, 10, 50 and 100 µm, another steps as 0.5 to 90 µm.
What does the debris actually do?
Commissioning debris is the documented enemy. New piping hides weld slag, mill scale, rust, sand and leftover construction debris. Start up without removing it and the literature’s warning is that it damages valve seats and trim during start-up — the failure mode is not gradual.
Particles are a leading cause of early instrument failure, and the worst of them arrive in the first weeks of a new system’s life.
Maintenance events re-inject the problem. Every opened fitting admits chips and scale, and a shred of PTFE tape broken off inside a port becomes a lodged contaminant.
Instrument makers describe the consequences in their troubleshooting notes: debris blocks pressure ports, wedges between plug and seat, cuts seating surfaces, and produces inaccurate readings or outright failure.
| Symptom | Most likely cause | What to change |
|---|---|---|
| Transmitter reads high, low or drifts, then settles after a flush | Debris lodged in the sensing port | A filter at the take-off, fine enough for the port |
| Valve will not seat, or leaks past the plug after start-up | Particles wedged between plug and seat, seating surfaces cut | The filter goes upstream of the valve, not downstream |
| Analyzer sensor fouls or drifts off calibration | Particulate or condensable carry-over into the sample | A coalescing or particulate stage ahead of the sensor |
| Element ΔP climbs in days rather than months | Grade too fine for the dirt load | A coarser element, or a strainer ahead of the fine element |
| Debris found in a line that was clean at commissioning | Chips, scale or a PTFE shred admitted at an opened fitting | Filter at every take-off, and cap open ends during work |
| Gauge lies, or a snubber or orifice blocks | Debris reaching the fine restriction because the filter sits downstream of it | Move the filter ahead of the snubber and any fixed orifice |
The cheap, effective defence is a barrier at the take-off: one inline filter per instrument leg, cheaper by orders of magnitude than the transmitter behind it.
For loops that also fight pulsation, the gauge snubber and orifice union complete the protection set.
Four cheap parts standing in front of one expensive instrument is the whole strategy — a filter at the take-off, a snubber where the process pulses, an orifice where flow must be capped, a manifold for isolation. The filter is the particle barrier among them.
Where does it go in the line?
Placement follows the threat. Filter at the take-off, where the leg leaves the process, because that is where the debris enters.
Filter upstream of regulators and control valves. Seat damage from particles is their classic failure, and several maker installation guides put the filter explicitly ahead of the regulator for that reason. Filter ahead of the analyzer sensor in sampling service too, where a coalescing or particulate stage is standard practice.
Order within the protection chain is engineering logic rather than a codified rule. Debris destroys porous snubber elements and clogs fixed orifices, so the filter belongs upstream of both — the barrier sits where it keeps the finer restrictions alive.
Check the drawing against four conditions:
- A filter on every instrument leg at the take-off — not only on the legs that look dirty.
- A filter ahead of every regulator and control valve seat.
- A filter ahead of every porous snubber and fixed orifice.
- A filter ahead of every analyzer sensor in sampling service.
Manifold-based hook-ups fold the filter into the block hardware, per the instrument manifold layout.
When do I change the element?
A clean element barely notices the flow; a loading element starts charging rent. Differential pressure is the service meter: baseline it clean, watch it climb, and replace at the maker’s recommended maximum.
The filter references are consistent that rising ΔP is the element-change signal, and that time-based replacement is the blunt alternative. Non-cyclable plants should treat elements as scheduled spares: one box per rating, swapped on ΔP or inspection.
Sintered elements are technically cleanable — backflushing, solvent or ultrasonic treatment all appear in maker procedures. In small inline bodies the element costs less than the labour to clean it, so replacement is the honest default.
- Baseline ΔP with a clean element at installation.
- Watch the climb — rising differential pressure is the change signal.
- Replace at the maker’s recommended maximum.
- Keep one box per rating on the shelf; it is a consumable, not a spare part.
- Where no gauge exists, use cycle time and response drift as the proxies.
What do I put in the RFQ?
Five lines carry the enquiry, and the maker maps the grade from the service line:
element grade— the protection job, e.g.10 µm for transmitter port protection, or the maker’s grade letter.body material and class—316, 6000 psigor the plant standard.ends— NPT/BSP thread or tube fitting, both sides.service— what flows and how dirty it starts: the maker sizes the grade from this.protected instrument— the model and its smallest passage, where you are unsure of the grade.
The grade line is the one that matters. Everything else the maker can confirm at order entry; a wrong grade protects the wrong thing.
FAQ
Can I clean and reuse a sintered element?
Yes — backflushing, solvent and ultrasonic cleaning are published procedures; the element survives many cycles. But a small element costs less than the labour to clean it. Clean in place only where the element is large, expensive or hazardous.
What micron rating do I need for a pressure transmitter?
Match the rating to the smallest passage it protects. Transmitter ports and valve trim gaps are the fine end — single-digit micron sintered elements. For bulk protection upstream of a regulator seat, mid-range mesh does the job.
Where does the filter go relative to the snubber?
Upstream. The snubber and any fixed orifice are the fine restrictions debris destroys, so the filter goes ahead of both. No standard codifies the order, but a clogged snubber lies about pressure.
How do I know when to change the element?
Differential pressure. Baseline it with a clean element, watch it climb, and change at the maker’s recommended maximum. Where no gauge exists, cycle time and response drift are the proxies.
Is a filter enough to protect the whole loop?
No. It stops particles, not pulsation or overpressure. Add a snubber where the process pulses, an orifice where flow must be capped, and a manifold for isolation.